- New
- Vielos tipas
- Pilnavidurė aplydymo viela
- Diameter (Ø)
- 1.2 mm
- Suvirinimo procesas
- MIG/MAG, aplydymas MAG būdu
- Vielos skersmuo
- 1,2 mm
- Vielos svoris
- 15 kg
- Ritės tipas
- B300, vielinė krepšinė ritė
- Klasifikacija pagal EN 14700
- S Fe 8
- Klasifikacija pagal DIN 8555
- MSG 6-GZ-60-S
- Medžiagos numeris
- 1.4718
- Aplydyto metalo kietumas be terminio apdorojimo
- 54–60 HRC
- Pirmojo sluoksnio ant nelegiruoto plieno kietumas
- Apie 53 HRC
- Srovės tipas ir poliškumas
- Nuolatinė srovė DC, viela jungiama prie teigiamojo poliaus (+)
- Apsauginės dujos pagal EN ISO 14175
- M12, M13, M21 arba C1
- Tipinė cheminė sudėtis
- C – 0,5 %; Si – 3,0 %; Mn – 0,5 %; Cr – 9,5 %; Fe – likutis
- Mechaninis apdirbimas po aplydymo
- šlifavimas
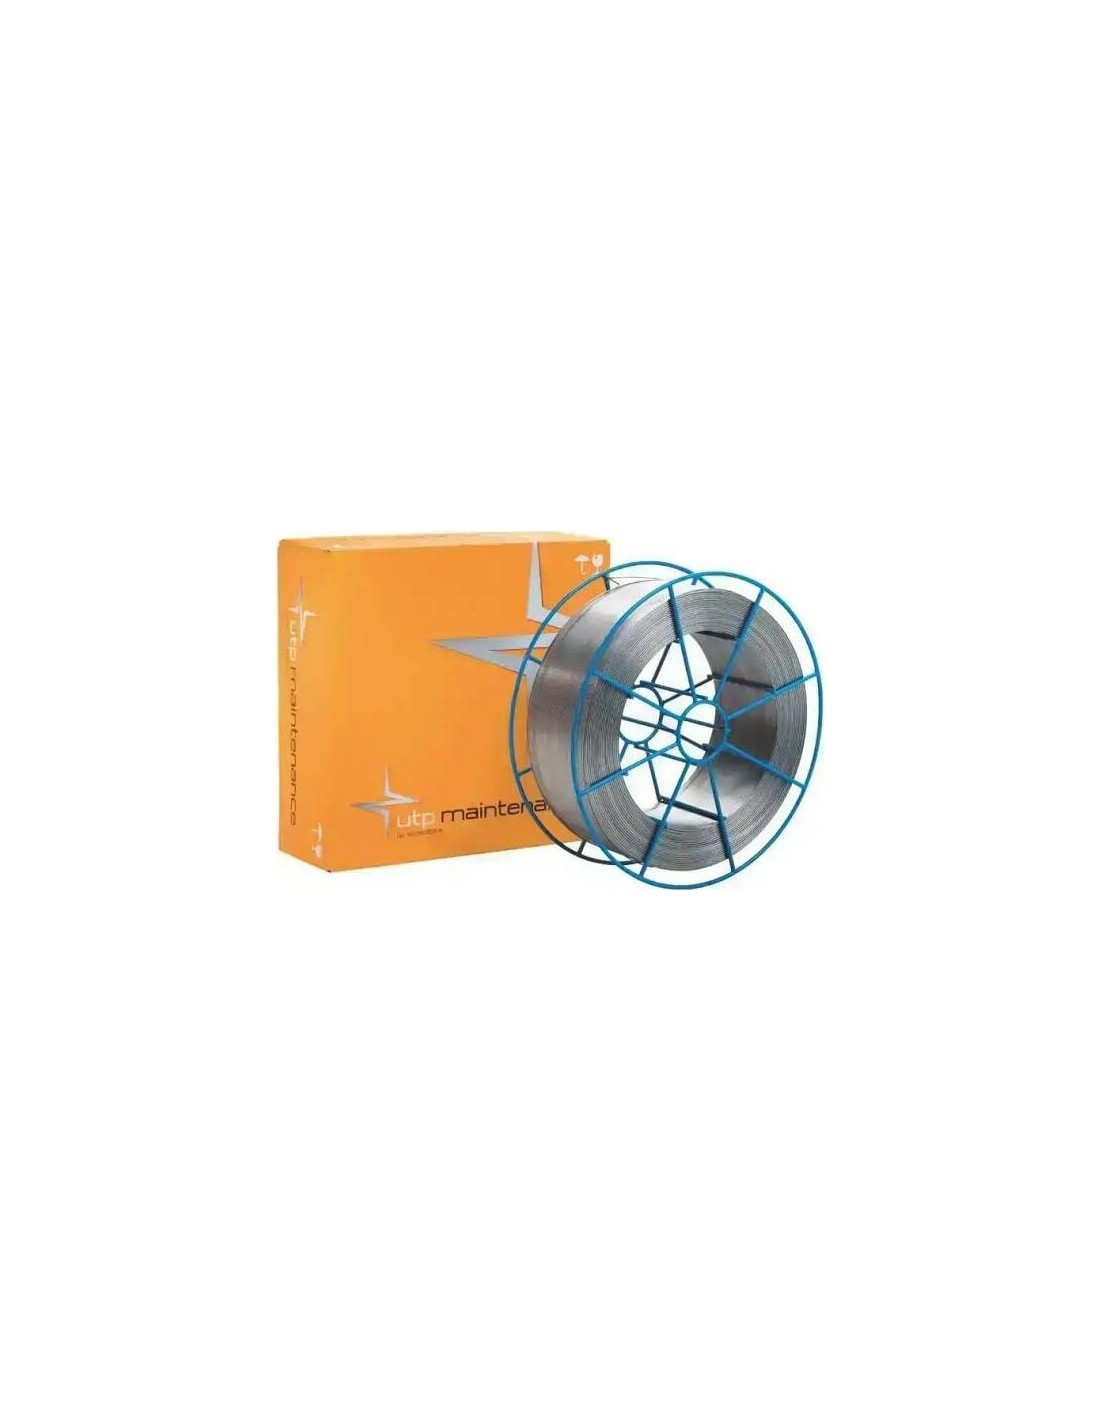
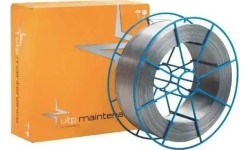
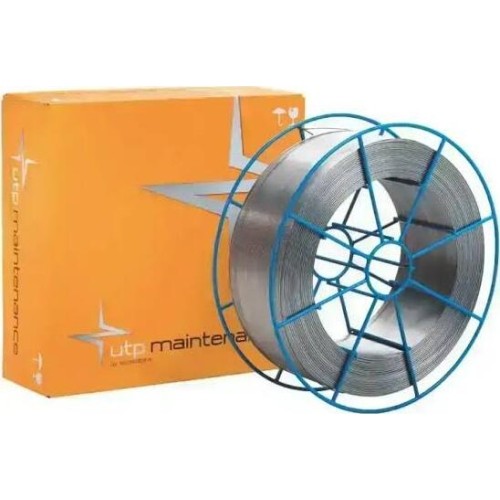
Welding wire Böhler WEARmig Dur 600, D300, 15kg - 1.2 mm
Description
UTP WEARmig Dur 600 - a solid MIG/MAG hardfacing wire designed for restoring worn metal part surfaces and forming a protective, wear-resistant layer. Suitable for parts subjected to high impact loads and moderate abrasive wear.
The weld metal has a hardness of 54-60 HRC while retaining toughness and crack resistance. It is a practical choice for equipment repair and maintenance when it is important to restore the working surface and increase its wear resistance.
Key benefits:
- Wear and impact resistance - the hard deposited layer protects heavily loaded surfaces.
- Restoration of worn surfaces - suitable for repair hardfacing and renewing the working layer of parts.
- Tough, crack-resistant weld metal - combines high hardness with resistance to mechanical loads.
- Wide industrial application - used for hardfacing parts of quarry, crushing, mining, steel and cement production equipment, as well as cutting tools and dies.
- 15 kg B300 spool - designed for use with compatible MIG/MAG wire feed equipment.
Application
The wire is intended for MAG hardfacing with shielding gas. Before work, the surface must be ground to clean metal. The need for preheating and the hardfacing parameters are selected according to the base metal and the part. The deposited layer can be machined by grinding.