- Maximum current MIG/MAG: 500
- Online only
- Free shipping
- Modelis
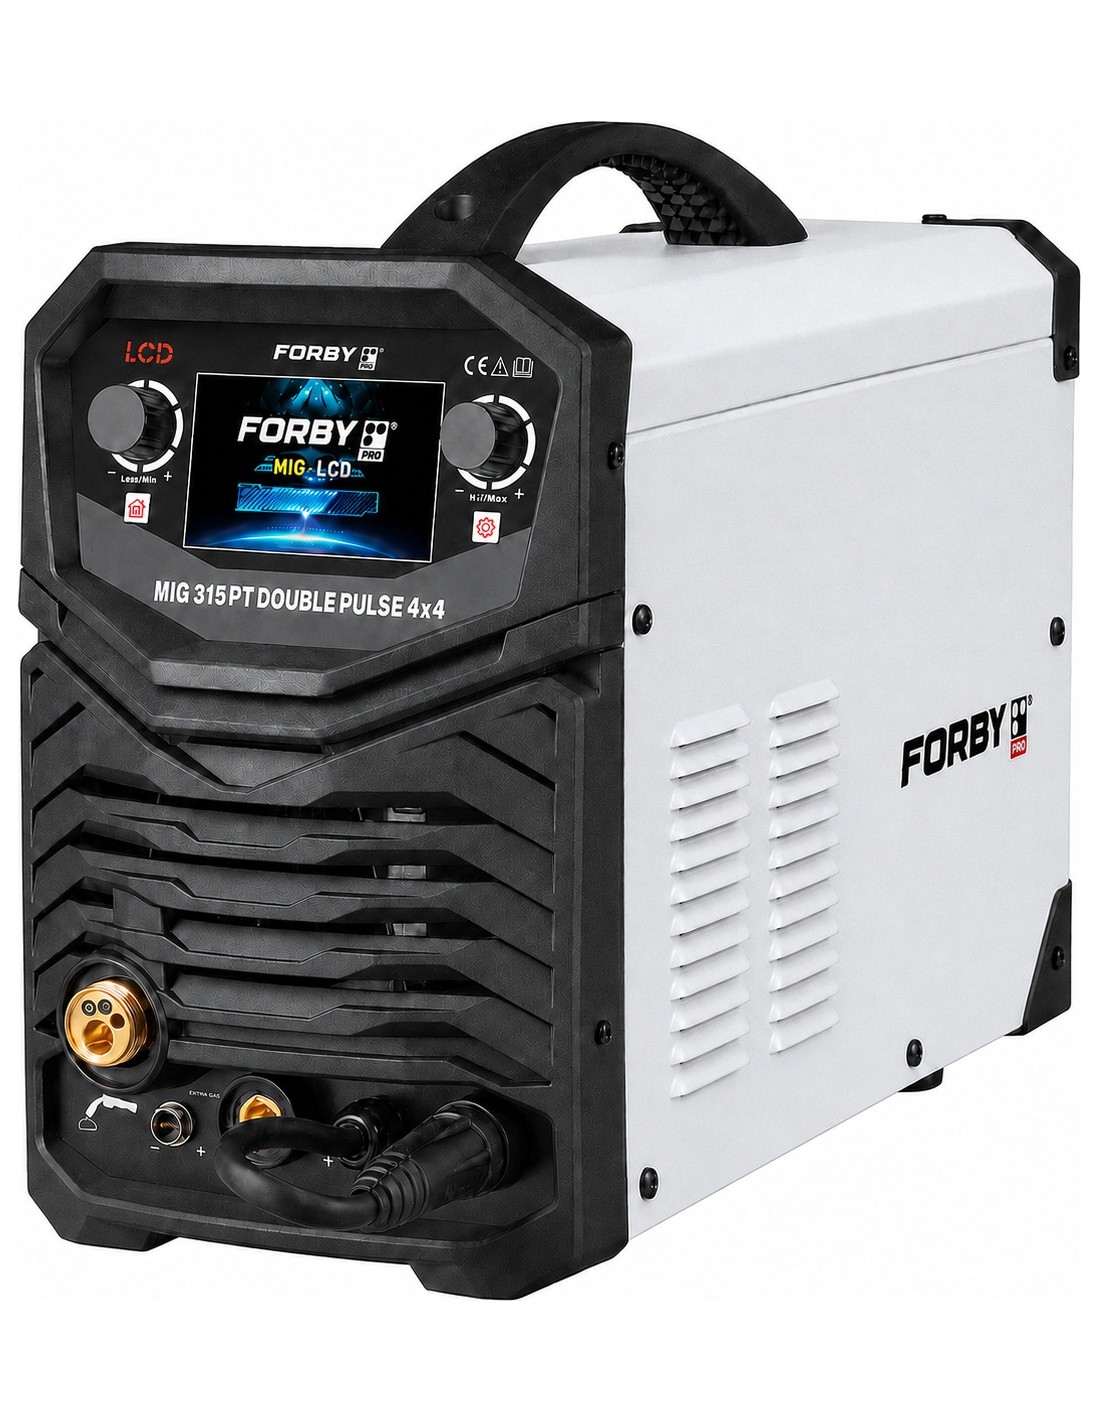
- FORBY® MIG 315PT Double Pulse 4x4.
- Apsaugos laipsnis
- IP21S
- Izoliacijos klasė
- H
- VRD
- įjungiama / išjungiama.
- Technologija
- IGBT inverterinė.
- MMA Darbo ciklas
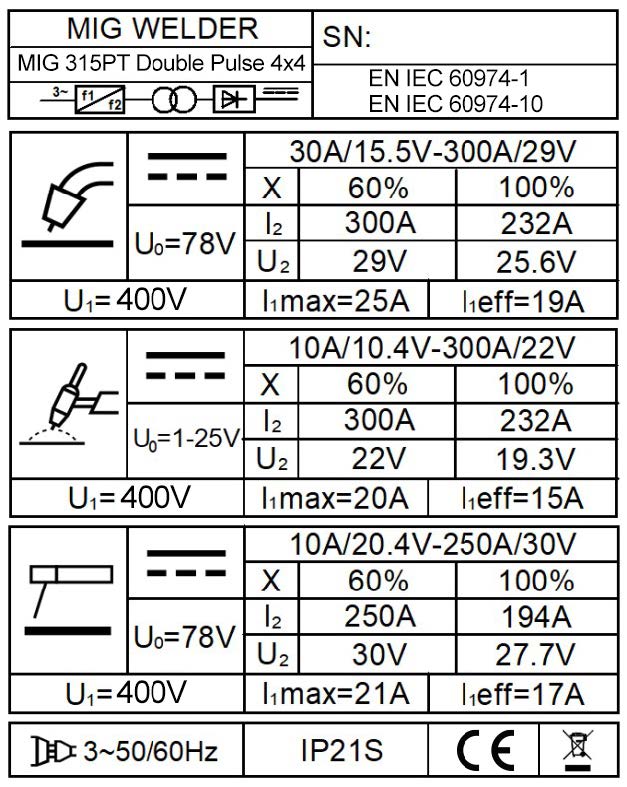
- 60 % prie 250 A; 100 % prie 194 A.
- Phase
- Trifazis (400V)
- Control
- synergetic
- Maitinimas
- Trifazis, 400 V, 50/60 Hz.
- User Level
- for workshops and small businesses
Professional - Aušinimas
- Oru, ventiliatoriumi.
- Weight, kg
- 22.5
- Wire spool size [kg]
- 5
15 - MIG/MAG darbo ciklas [%]
- 60 % prie 300 A; 100 % prie 232 A.
- PFC function
- No
- Maximum current MIG/MAG
- 300
- MMA Srovės diapazonas
- 10–250 A.
- Suvirinimo režimai
- MIG/MAG, Single Pulse MIG, Double Pulse MIG, MMA, Lift TIG DC.
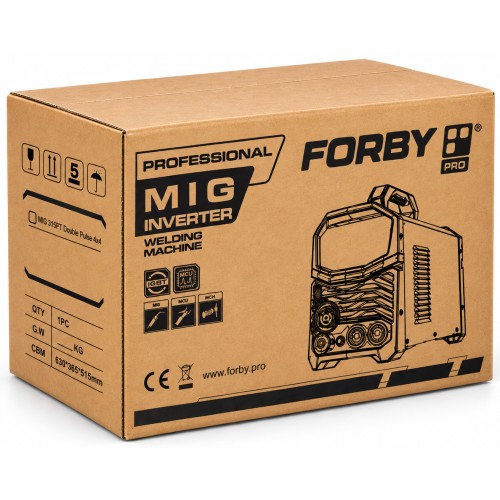
- Pakuotės matmenys
- 630 × 365 × 515 mm.
- Inverter technology
- IGBT
- Shielding Gas Requirement
- Gas / Gasless
- Number of wire feed rollers
- 4
- Torch length
- 3 m
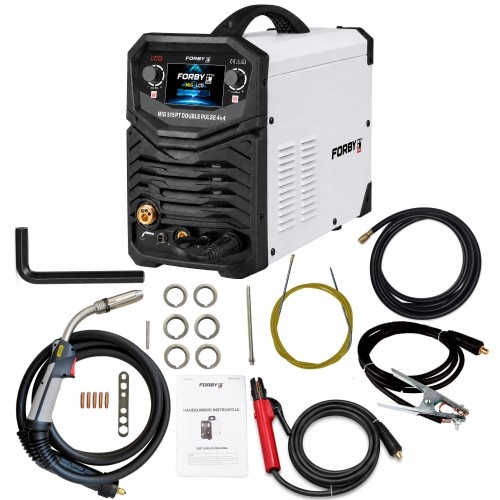
- Package Contents
- consumable parts
electrode cable
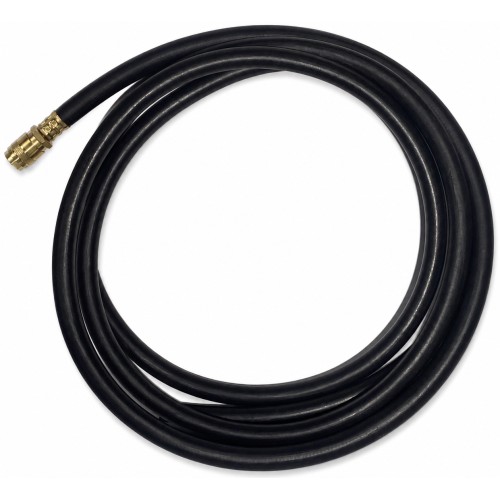
gas hose
ground cable
MIG / MAG burner
plieninis šarvas
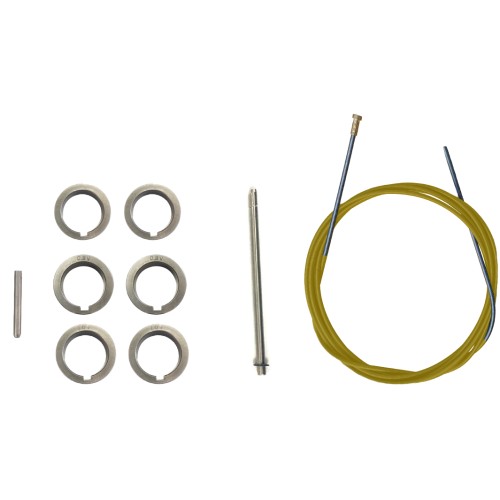
teflono įdėklas
welding machine - Ground cable connection
- big (35 - 50 mm)
- Torch connection in the machine
- EURO
- Functions
- 2T / 4T
ARC FORCE
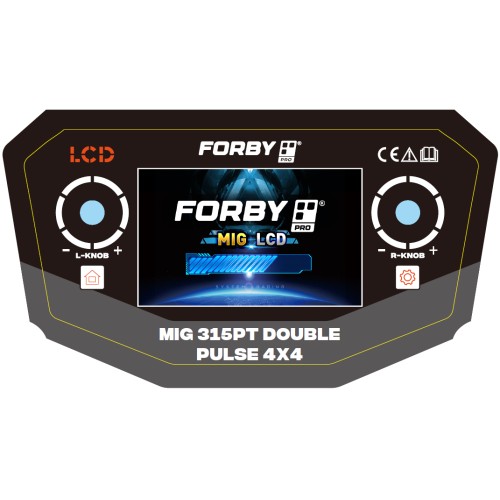
digital display
DOUBLE PULSE
FLUX (be dujų)
Lift TIG
PULSE
VRD - Welding methods
- MIG FLUX (without gas)
MIG single & double PULSE
MIG/MAG welding
MMA (electrodes)
TIG Lift - Aparato matmenys
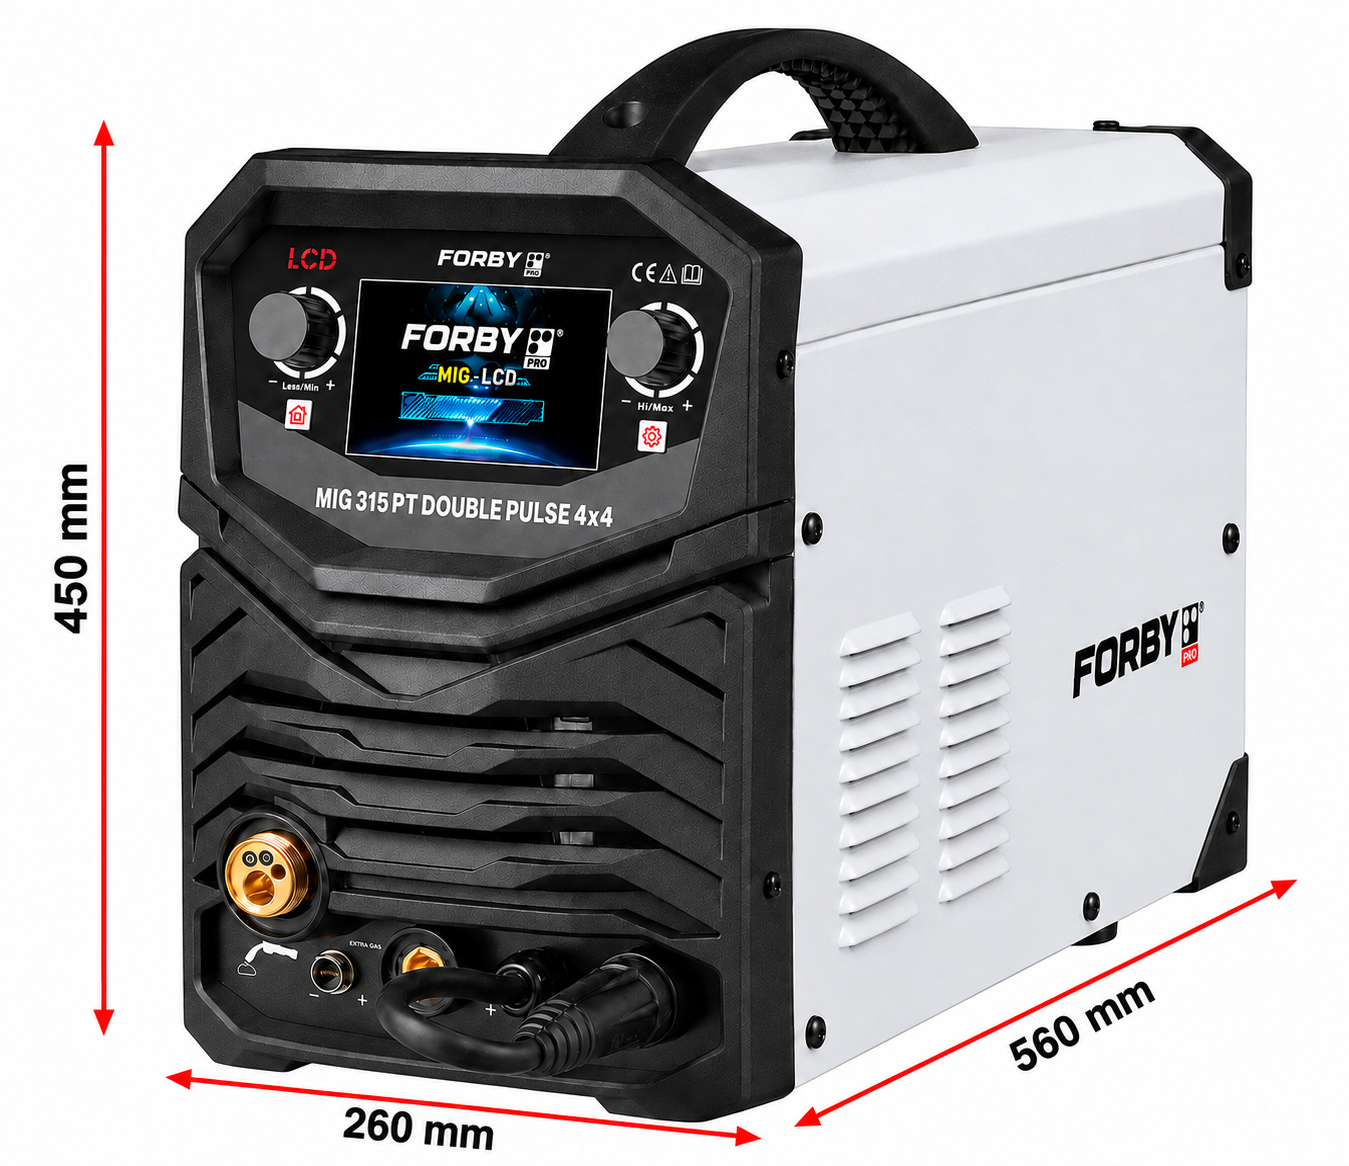
- 560 × 255 × 445 mm.
- Ekranas
- 5″ LCD.
- Suvirinimas savisauge milteline viela
- Galimas, parinkus tinkamą vielą ir padavimo dalis.
- MIG/MAG srovės diapazonas
- 30–300 A.
- Lift TIG srovės diapazonas
- 10–300 A.
- Lift TIG darbo ciklas
- 60 % prie 300 A; 100 % prie 232 A.
- Darbo ciklo vertinimas
- 10 minučių ciklas, 40 °C aplinkos temperatūra.
- MIG/MAG vardinė išėjimo įtampa
- 15,5–29 V.
- Lift TIG vardinė išėjimo įtampa
- 10,4–22 V.
- MMA vardinė išėjimo įtampa
- 20,4–30 V.
- MIG įėjimo srovė I1max / I1eff
- 25 / 19 A.
- Lift TIG įėjimo srovė I1max / I1eff
- 20 / 15 A.
- MMA įėjimo srovė I1max / I1eff
- 21 / 17 A.
- Tuščiosios eigos įtampa MIG / MMA
- 78 V.
- Tuščiosios eigos įtampa Lift TIG
- 1–25 V.
- Sinerginis valdymas
- Yra.
- COOL PULSE
- Automatinis įjungimas viengubo pulso režimu, kai vielos padavimo greitis mažesnis nei 2,5 m/min.
- MIG įtampos korekcija
- Nuo –5 iki +5 V.
- Induktyvumo reguliavimas
- Nuo –10 iki +10.
- Degiklio valdymas
- 2T / 4T.
- Hot Start reguliavimas
- 0–10.
- Arc Force reguliavimas
- 0–10.
- EMC plokštė
- Yra.
- Vielos padavimo mechanizmas
- Keturių ritinėlių.
- Vielos ritės
- 5 kg ir 15 kg.
- Vielos skersmenys
- 0,8 / 0,9 / 1,0 / 1,2 mm, pagal programą.
- Aliuminio vielos skersmenys pagal programas
- 1,0 / 1,2 mm.
- MMA elektrodų skersmenys pagal instrukciją
- 2,5 / 3,2 / 4,0 / 5,0 mm.
- Dujų žarna
- 3 m, greitoji jungtis NW5, vidinis / išorinis skersmuo 6 / 13 mm.
Welding machine 315PT Double Pulse 4x4
Description

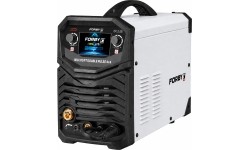
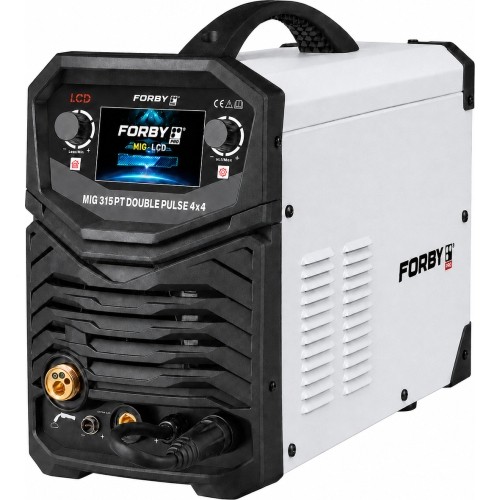
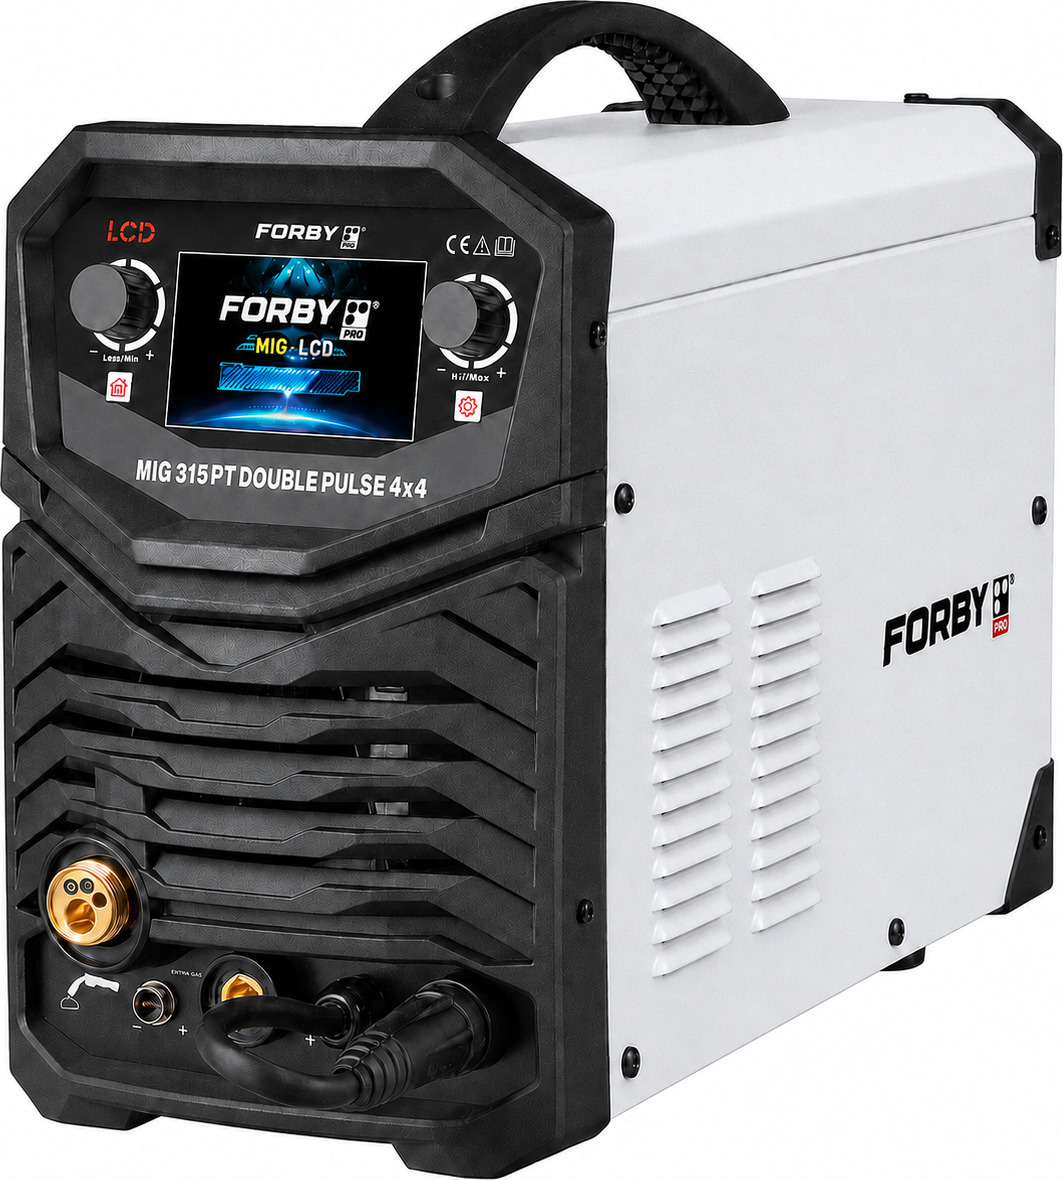
Inverter welding machine FORBY® MIG 315PT Double Pulse 4x4 (300 A - 60 %) (three-phase 400 V)
Double pulse, four-roller wire feed and a 5-inch LCD display - for productive and precisely controlled welding.
FORBY® MIG 315PT Double Pulse 4x4 is a three-phase inverter welding machine designed for MIG/MAG, single and double pulse MIG, MMA and Lift TIG welding. In MIG and Lift TIG modes it delivers up to 300 A, and in MMA mode up to 250 A welding current.
Why choose this model?
- 300 A / 60 %: in MIG and Lift TIG modes, at 40 °C.
- Double Pulse: more control over bead formation and heat input.
- 4x4 wire feed: four rollers for even wire feeding.
- Synergic control: automatic matching of wire feed speed and voltage.
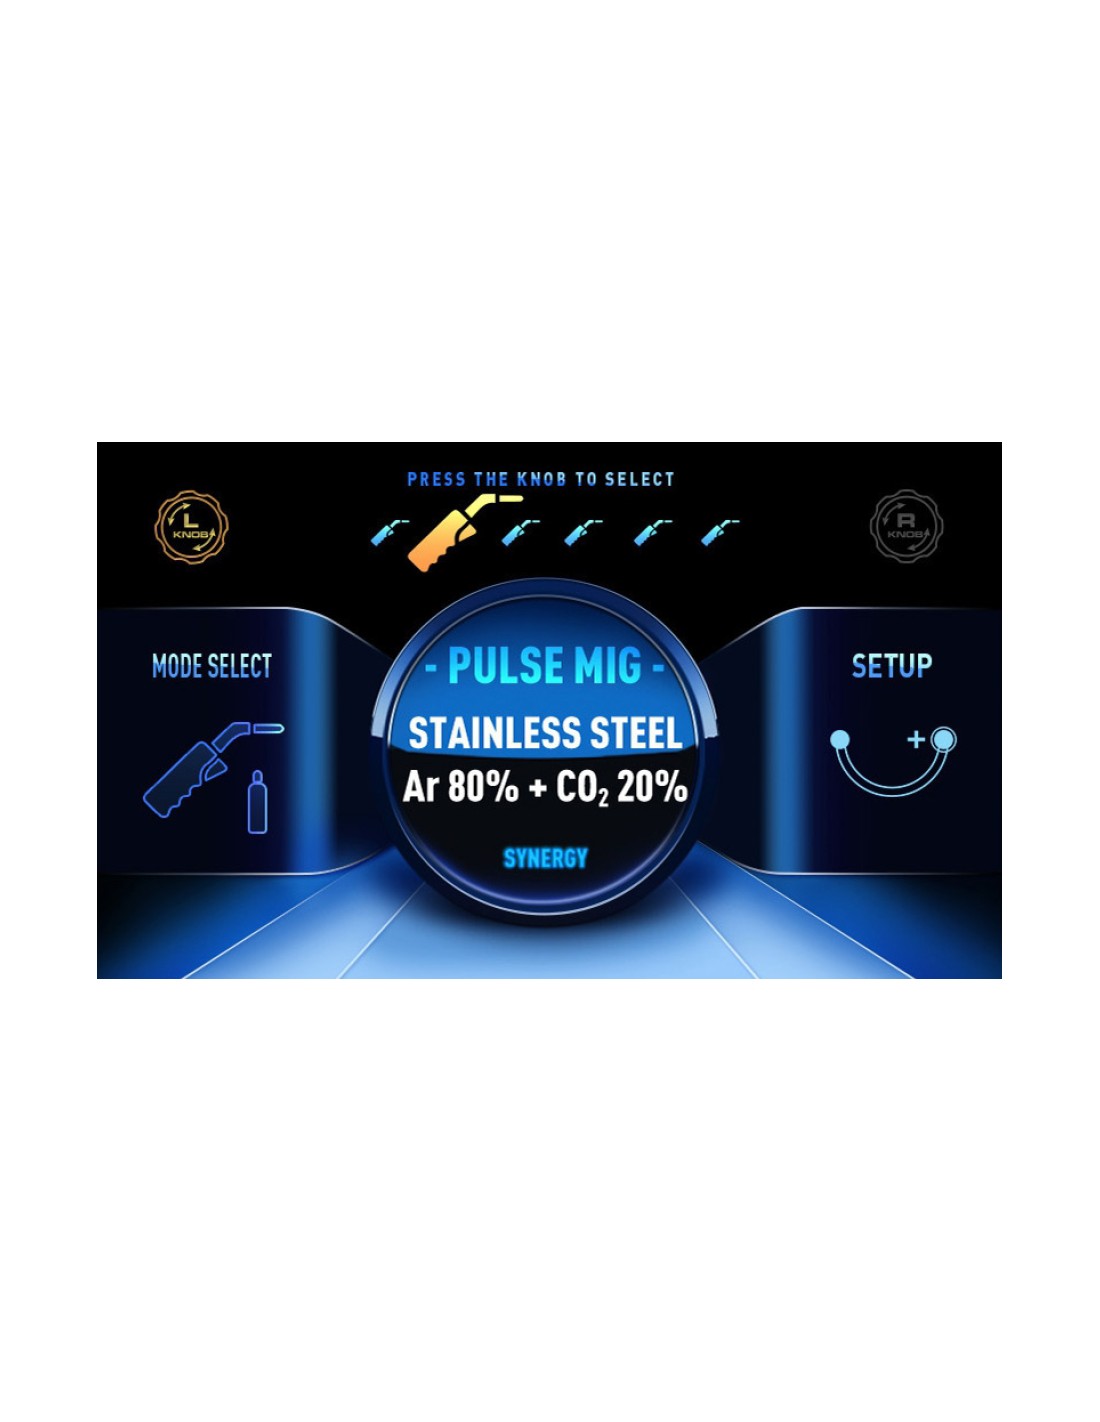
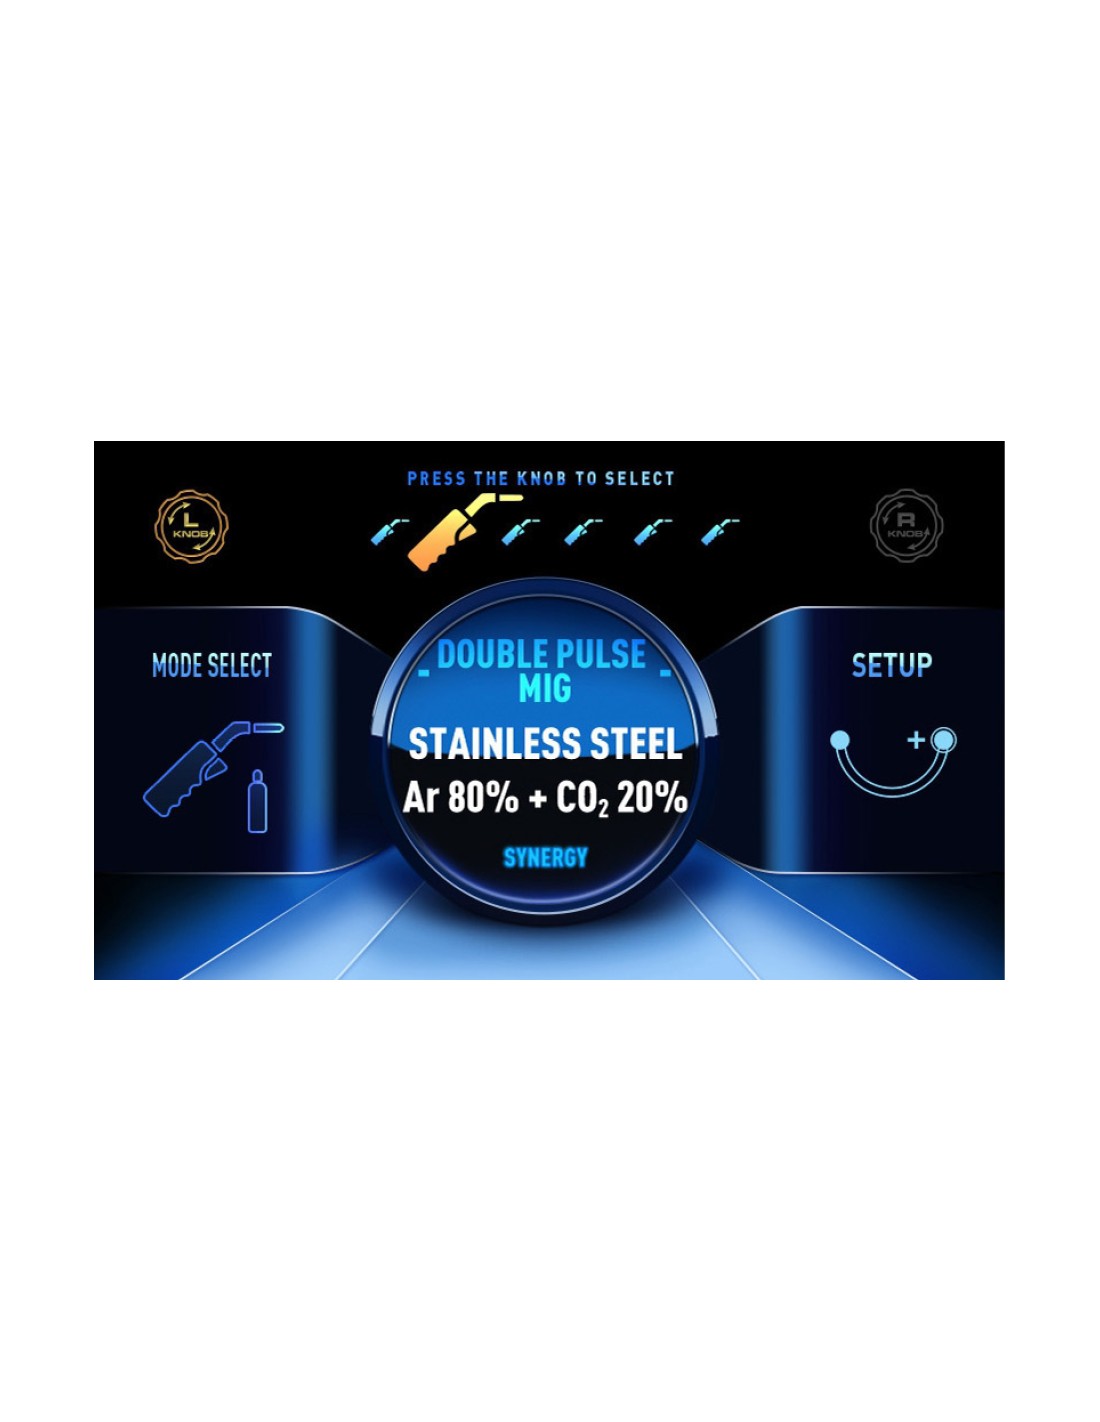
- 5″ LCD display: convenient control of modes and parameters.
- 5 and 15 kg wire spools: choose according to the scope of work.
- EMC board: for reducing electromagnetic interference.
A versatile choice for repair workshops, metal fabrication and welding of various structures.

IGBT inverter technology and EMC board
The machine uses IGBT inverter technology. The high-frequency power converter makes it possible to control welding energy and adapt the machine's operation to different welding processes.
Electronic control and a feedback circuit help maintain the set parameters and a stable arc. The synergic system matches wire feed speed and welding voltage, while additional corrections allow the arc to be fine-tuned for the job.
What is EMC?
EMC (Electromagnetic Compatibility) - electromagnetic compatibility. It describes the ability of equipment to operate in an electromagnetic environment without causing unacceptable interference to other equipment and while maintaining proper operation when exposed to external interference.
This model is fitted with an EMC board designed to reduce electromagnetic interference. The inverter controls power conversion, the synergic system matches welding parameters, and the EMC board performs the interference reduction function.
Welding modes and their purpose
MIG/MAG - wire welding
- Welding current range: 30-300 A.
- Standard synergic MIG, single pulse and double pulse modes.
- Welding with shielding gas or self-shielded flux-cored wire, with the correct polarity and feed parts selected.
- Wire diameters: 0.8 / 0.9 / 1.0 / 1.2 mm, depending on material and program.
MMA - welding with coated electrodes
- Welding current range: 10-250 A.
- Adjustable Hot Start and Arc Force functions.
- VRD function can be switched on and off.
- Electrode diameters according to the manual: 2.5 / 3.2 / 4.0 / 5.0 mm.
Lift TIG - direct current welding
- Welding current range: 10-300 A.
- The arc is ignited by touching the workpiece with the tungsten electrode and lifting it.
- A compatible TIG torch, argon, regulator and consumables are required.
For aluminium welding, this machine uses MIG mode with suitable wire, argon and an adapted wire feed system. Lift TIG mode is DC, without AC function.


Double Pulse - more bead and heat control
Single pulse - a mode in which the welding current alternates between a peak and a base value. Properly selected settings help control metal transfer into the weld pool and reduce spatter.
Double pulse additionally alternates groups of higher and lower energy pulses. The rhythmic change in energy gives more options for controlling the weld pool and heat input and for forming an evenly rippled bead surface.
- Useful when welding aluminium and for work where bead appearance matters.
- In double pulse mode, pulse frequency, pulse width and base current parameter are adjustable.
- Allows the process to be adapted to the material, workpiece thickness and welding speed.
The final result depends on the selected program, wire, gas, workpiece preparation and welding technique.

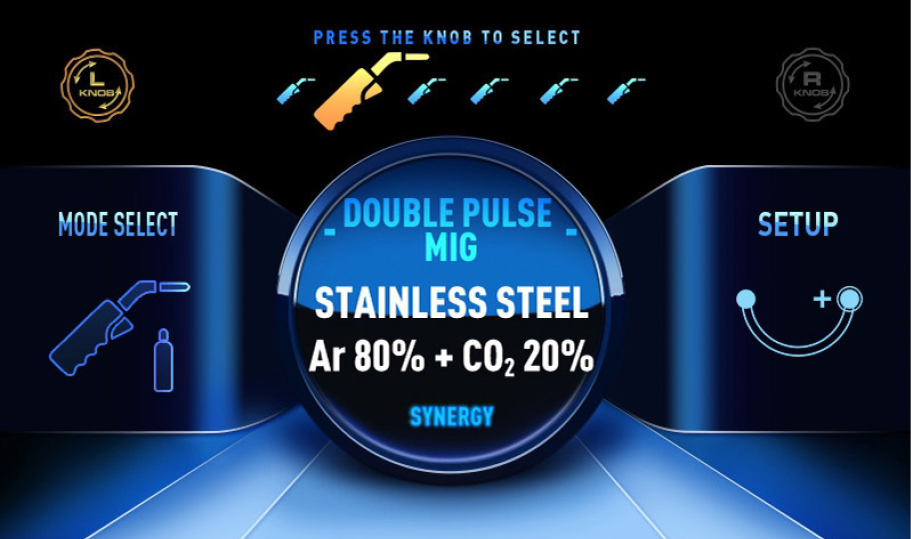
5″ LCD display and synergic control
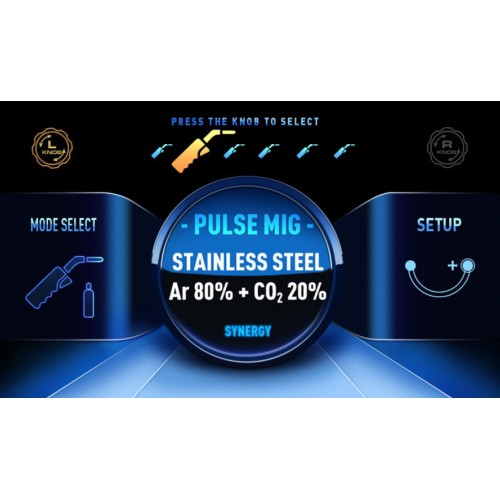
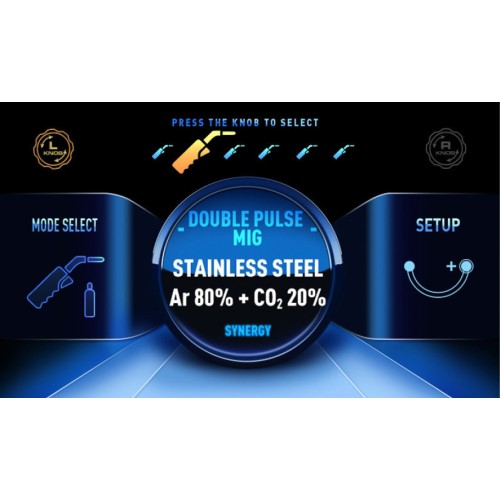
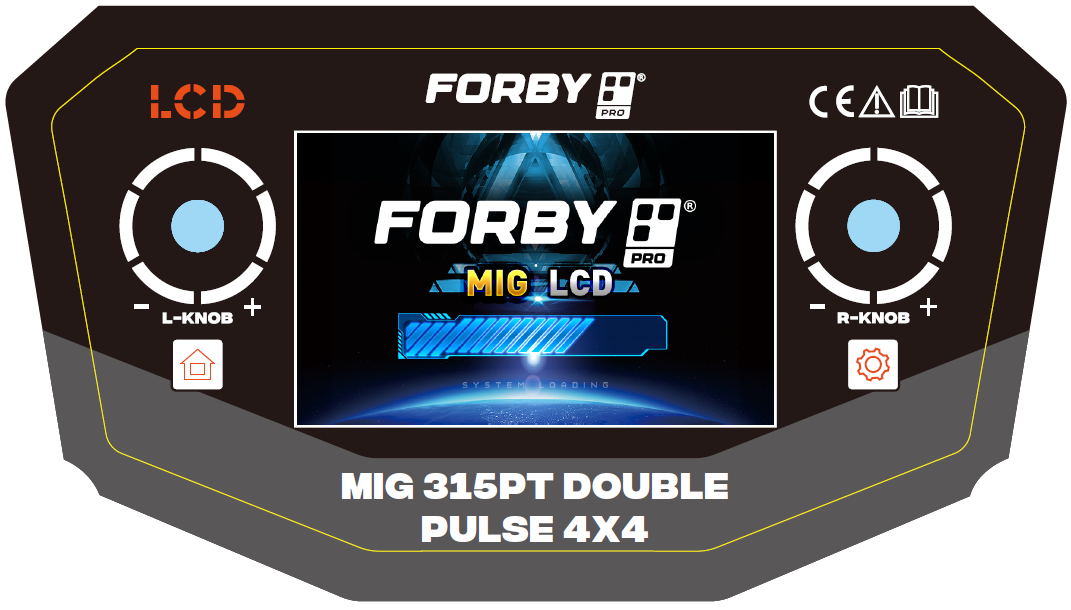
The 5-inch LCD display shows the settings of the selected mode. During welding, the actual welding current and voltage can be monitored.
Synergic control automatically matches wire feed speed and welding voltage according to the selected program. This simplifies initial setup, while voltage correction allows further fine-tuning of the arc.
- Selection of material, wire diameter and gas by program.
- MIG voltage correction: from -5 to +5 V.
- Inductance adjustment: from -10 to +10.
- 2T / 4T torch trigger control.
- Setting of slow wire feed during arc ignition.
- Adjustment of post-flow gas time.
According to the manual, in single pulse mode COOL PULSE switches on automatically when the wire feed speed is below 2.5 m/min. It is an additional pulse welding function for work at lower wire feed speeds.
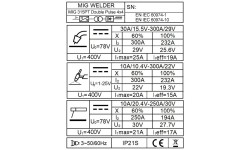
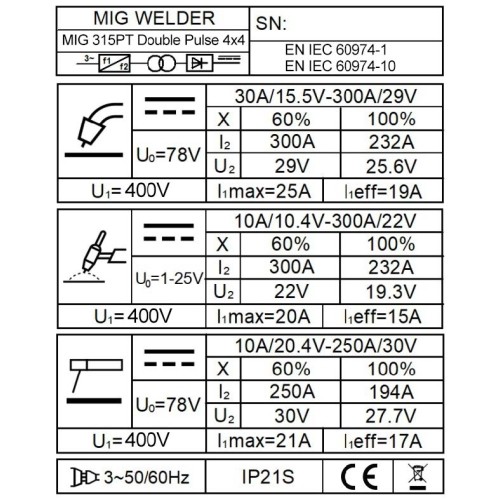
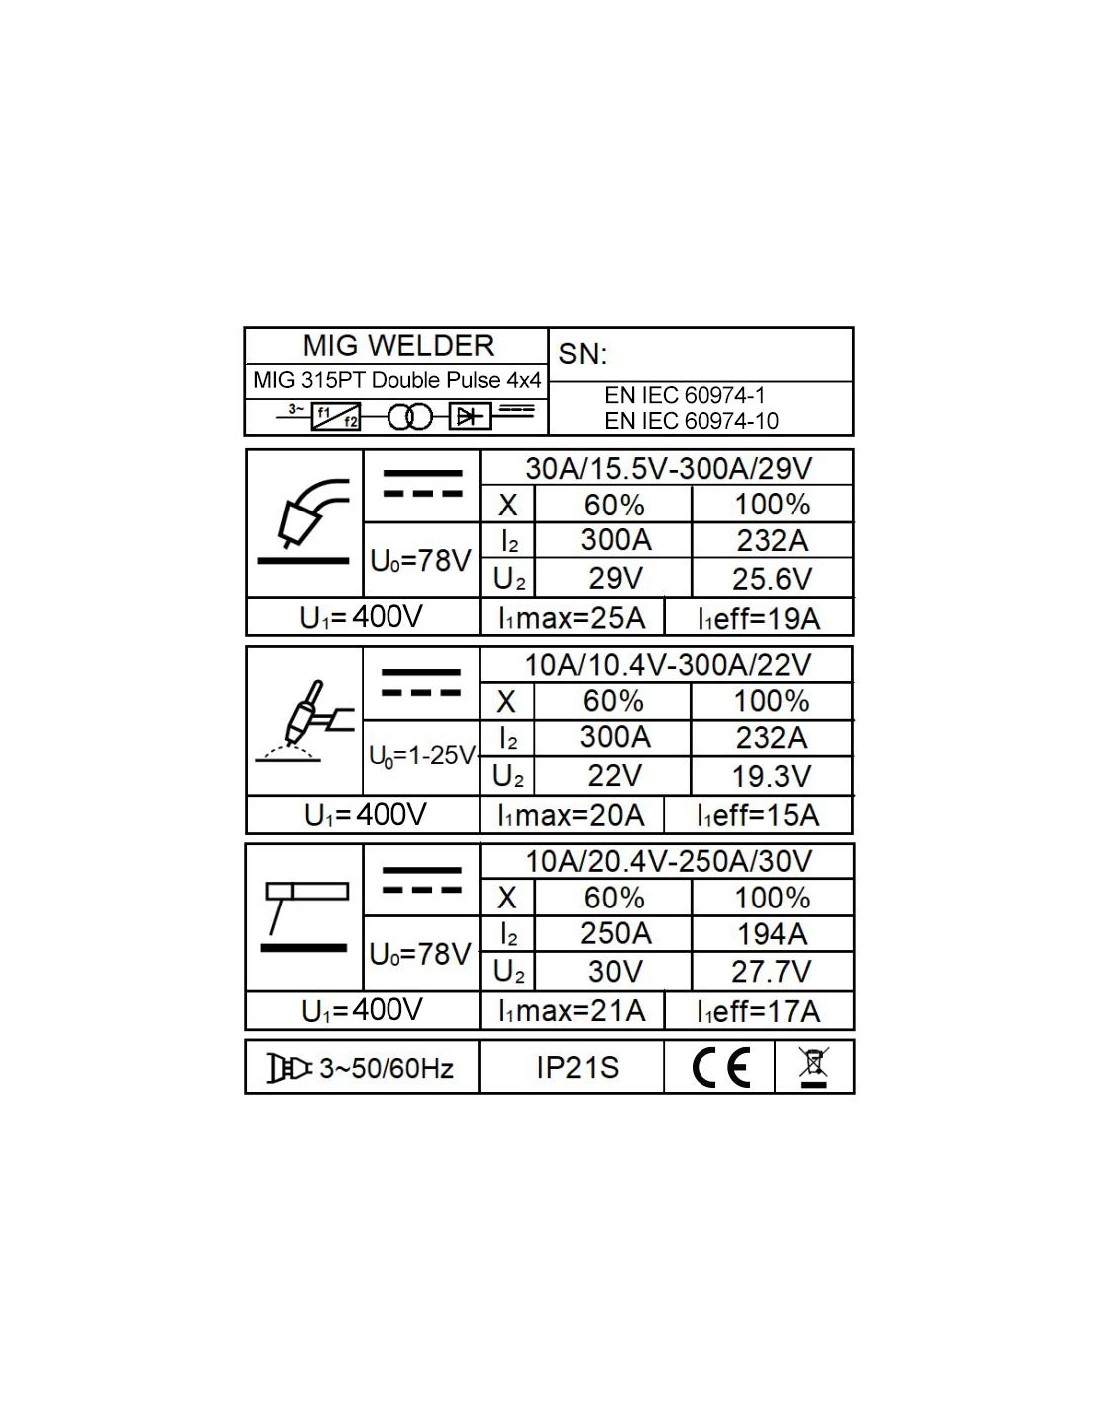
Duty cycle according to the machine's rating plate
The duty cycle indicates what portion of a 10-minute period can be spent welding at a given current. For this model, the 60 % duty cycle is specified at an ambient temperature of 40 °C.
| Mode | 60 % | 100 % |
|---|---|---|
| MIG/MAG | 300 A | 232 A |
| Lift TIG | 300 A | 232 A |
| MMA | 250 A | 194 A |
60 % at 300 A in MIG or Lift TIG mode means 6 minutes of welding and 4 minutes of cooling in a 10-minute cycle.
100 % duty cycle means continuous operation at the current given in the table under rated conditions. High ambient temperature or limited cooling may reduce the permissible load.

Programs for different materials
The manual provides programs for carbon and stainless steel, aluminium alloys and CuSi wire. In each case it is important to match the program, wire diameter, feed parts and shielding gas.
- Carbon steel: standard MIG/MAG, pulse modes and use of flux-cored wire according to the selected program.
- Stainless steel: pulse programs with suitable wire and gas mixture.
- Aluminium-silicon and aluminium-magnesium alloys: 1.0 / 1.2 mm wire, U-groove rollers and argon.
- CuSi wire: the manual provides single and double pulse programs with argon.

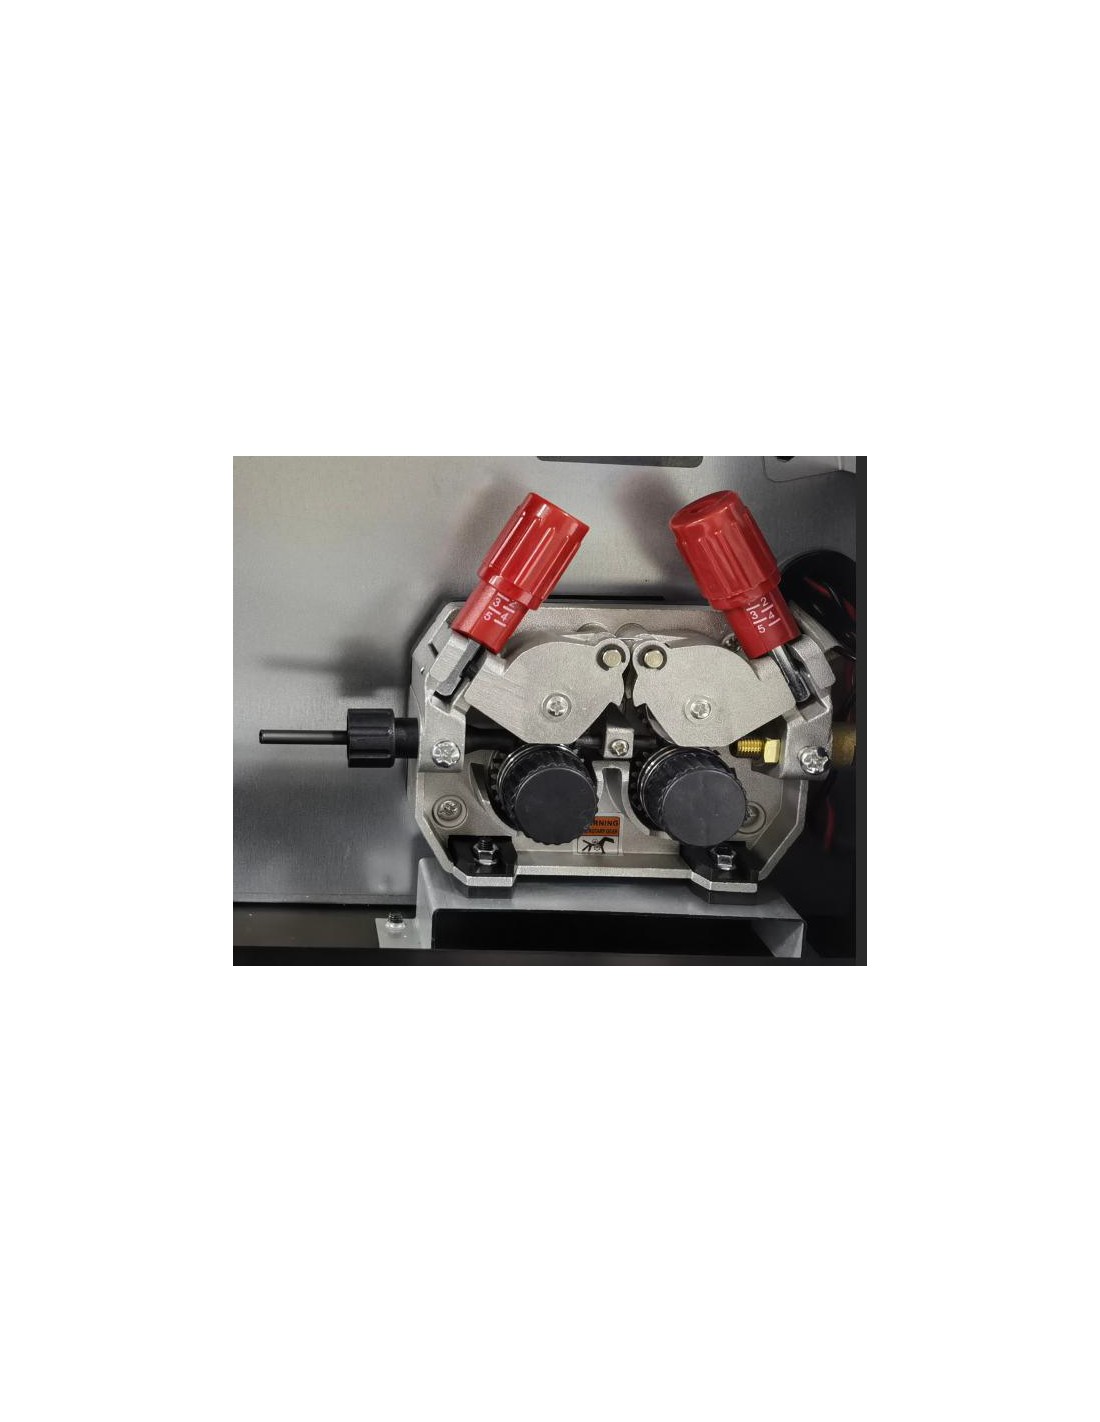
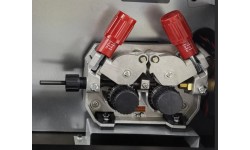
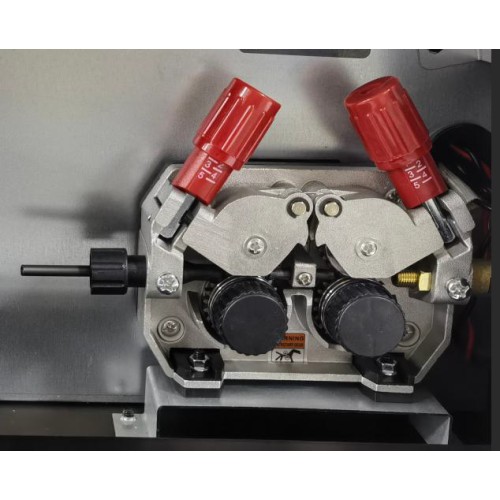
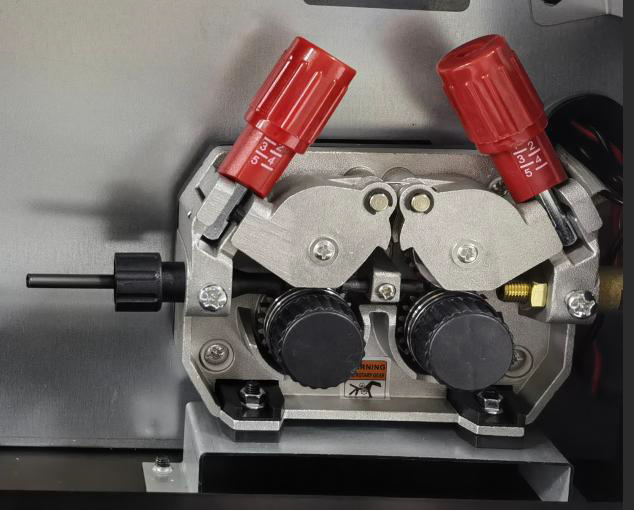
4x4 - four-roller wire feed mechanism
The four-roller mechanism helps feed the welding wire evenly to the torch. Correct pressure and roller profile are especially important when working with softer aluminium wire.
The machine accepts 5 and 15 kg wire spools. The opening side compartment gives access to the spool, wire feed mechanism and pressure adjustment.
- V-groove rollers: for steel wire.
- U-groove rollers: for aluminium wire.
- K-groove rollers: for flux-cored wire accordingly; they are not listed in the standard package.
The rollers, contact tip and torch liner must match the wire material and diameter. Excessive pressure can deform the wire and increase wear of the mechanism.
Dimensions and workplace preparation
The machine, with a net weight of 22.5 kg, houses the wire spool and the four-roller feed mechanism in one housing.
- Machine dimensions: 560 × 255 × 445 mm.
- Package dimensions: 630 × 365 × 515 mm.
- Cooling: forced air, using a fan.
- Side compartment for convenient access to the wire spool and feed mechanism.
- Connectors for the torch and welding cables located at the front.
Place the machine on a stable surface, do not cover the ventilation openings and leave at least 30 cm of free space around it for air circulation.


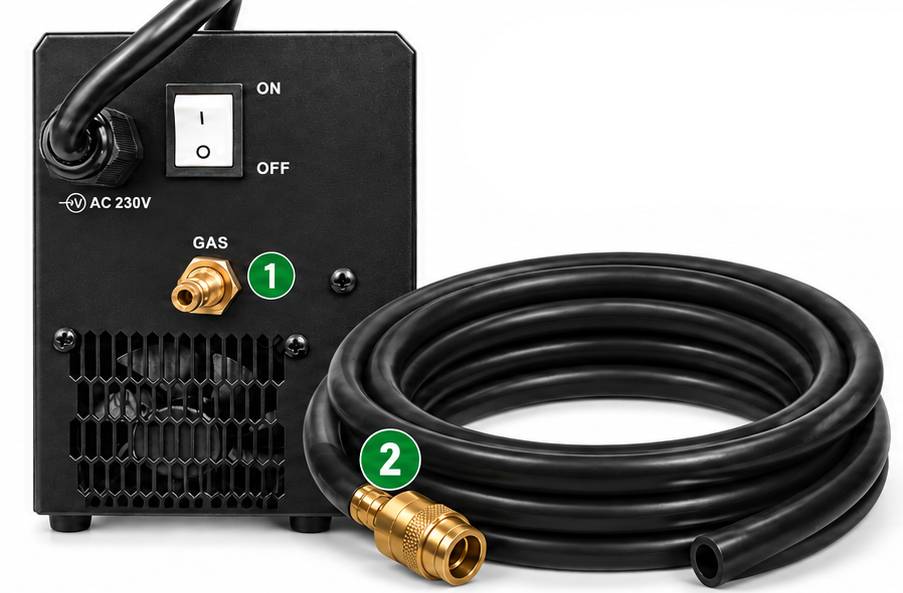
QUICK AND CONVENIENT GAS HOSE CONNECTION
1. The integrated quick gas coupling allows the gas hose to be connected or disconnected easily and quickly. This shortens the machine's setup time and makes moving and transporting it easier.
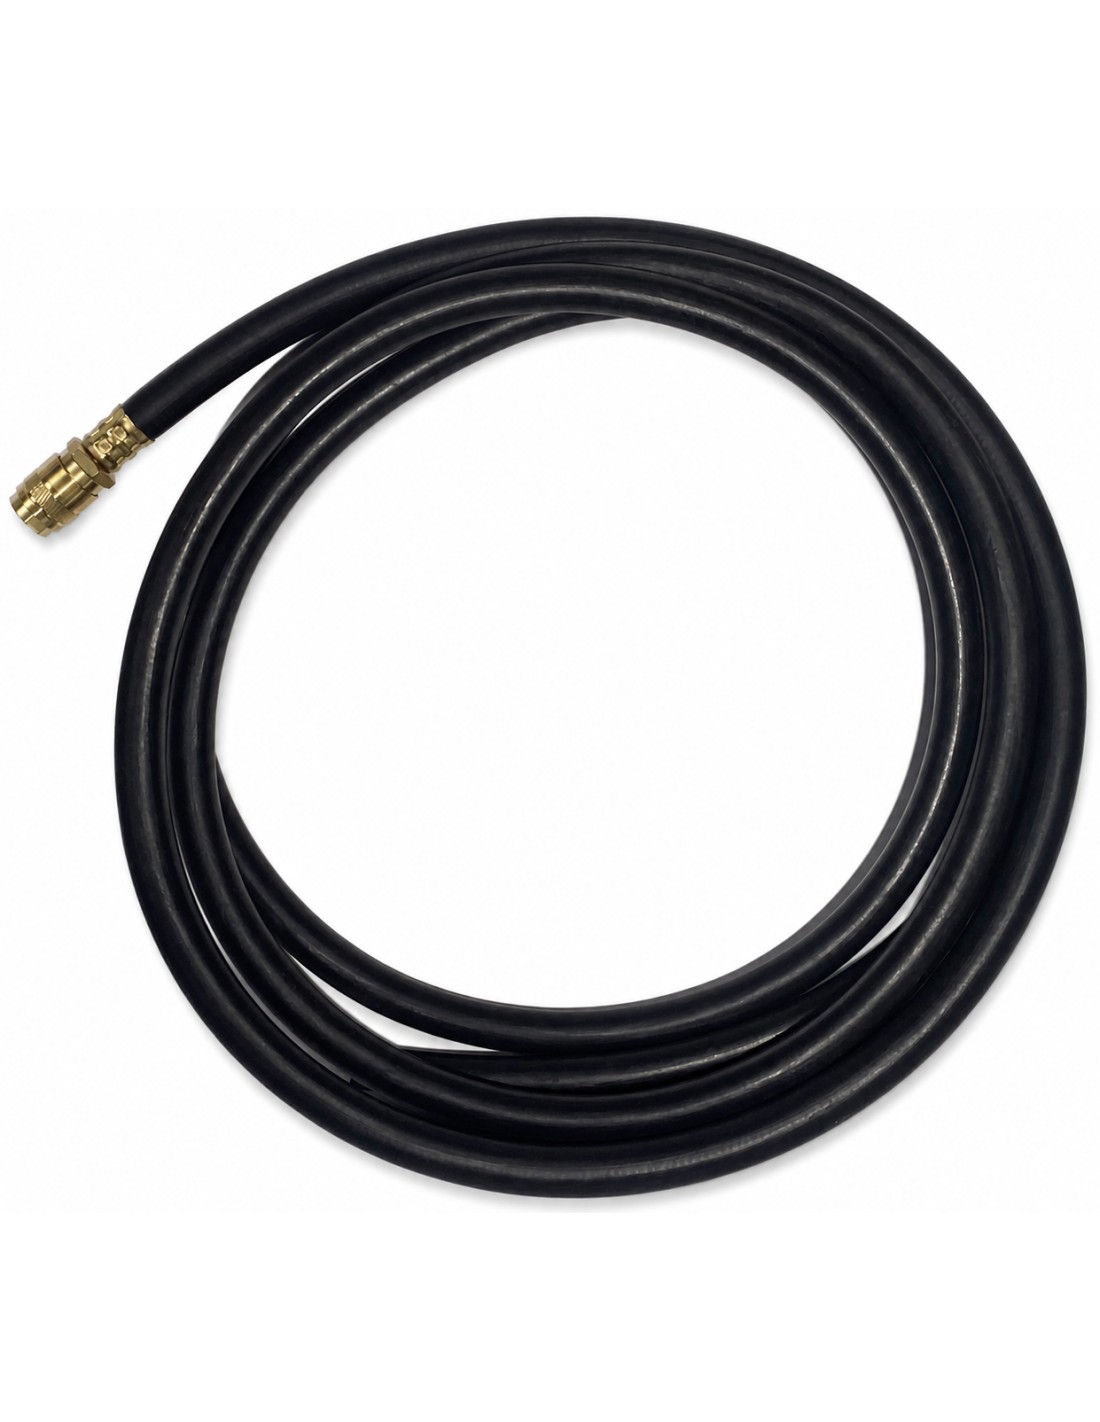
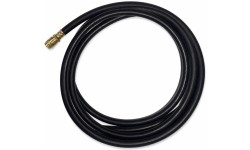
2. A 3-metre pressure-resistant gas hose is included with a quick coupling on the machine side. The optimal hose length gives more freedom to conveniently position the welding machine and gas cylinder at the workplace.
ROBUST CONNECTORS DESIGNED FOR HIGHER LOADS
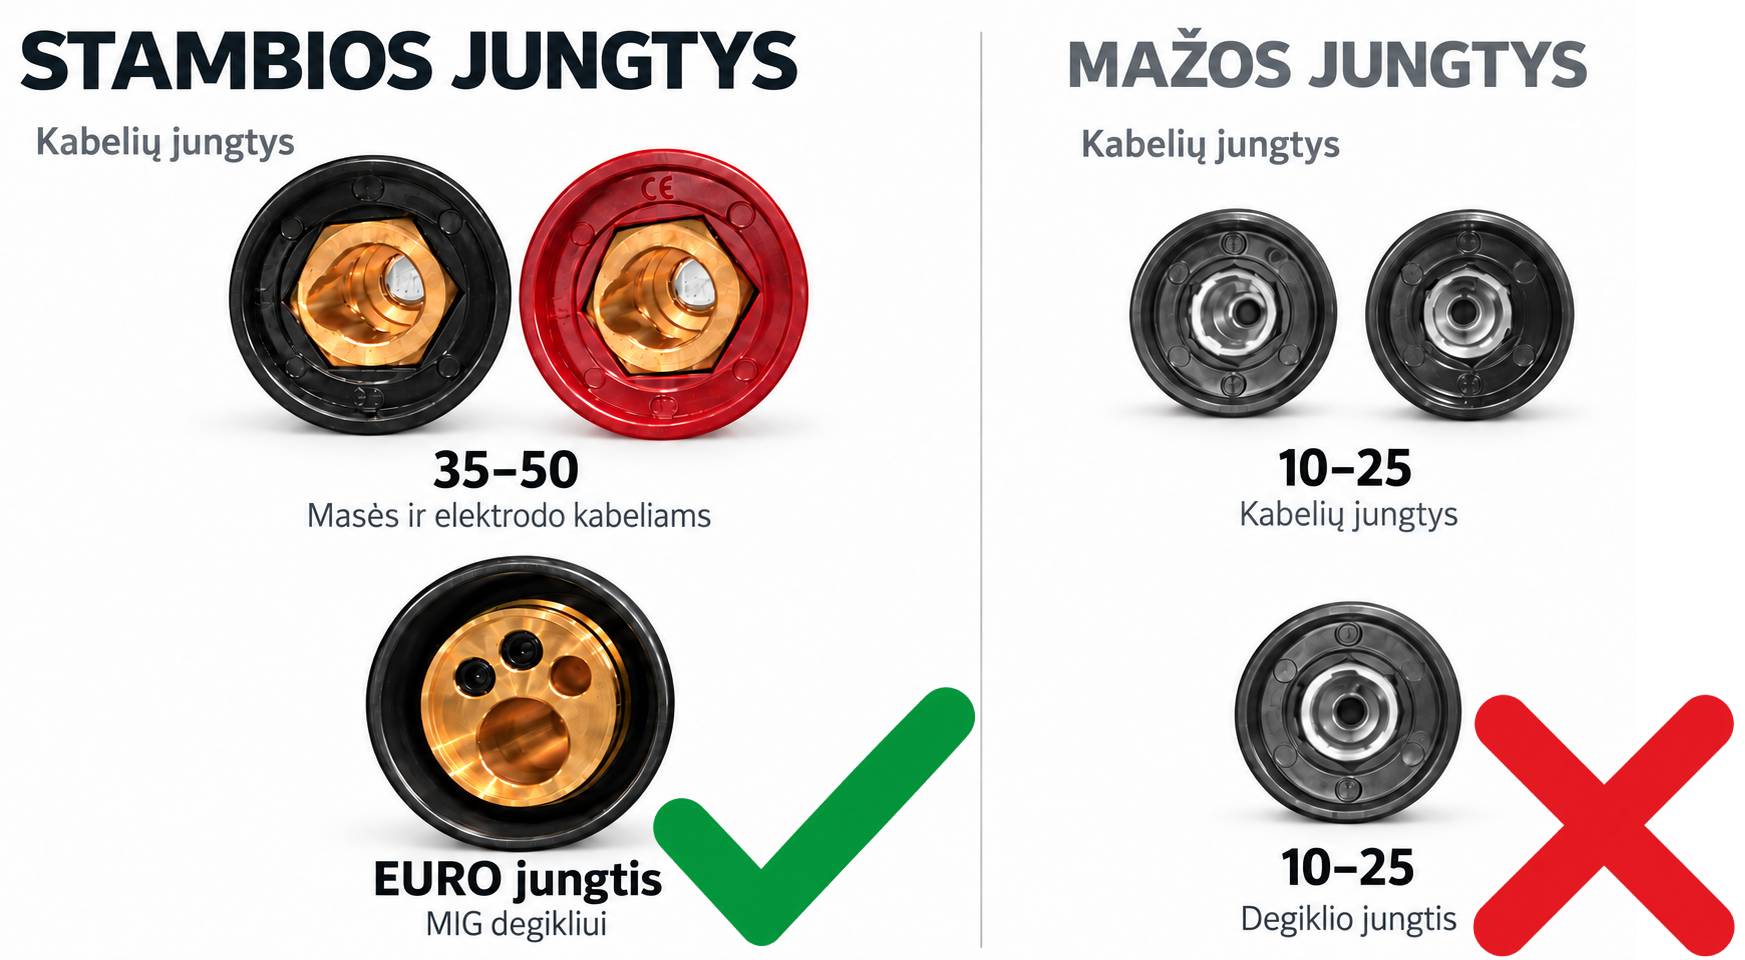
Large 35-50 welding cable connectors ensure reliable contact and stable current transfer. They are designed for higher loads and help reduce connector heating and energy losses. Compared to budget-class machines, which more often use 10-25 connectors, 35-50 welding cable connectors provide an extra reliability margin.
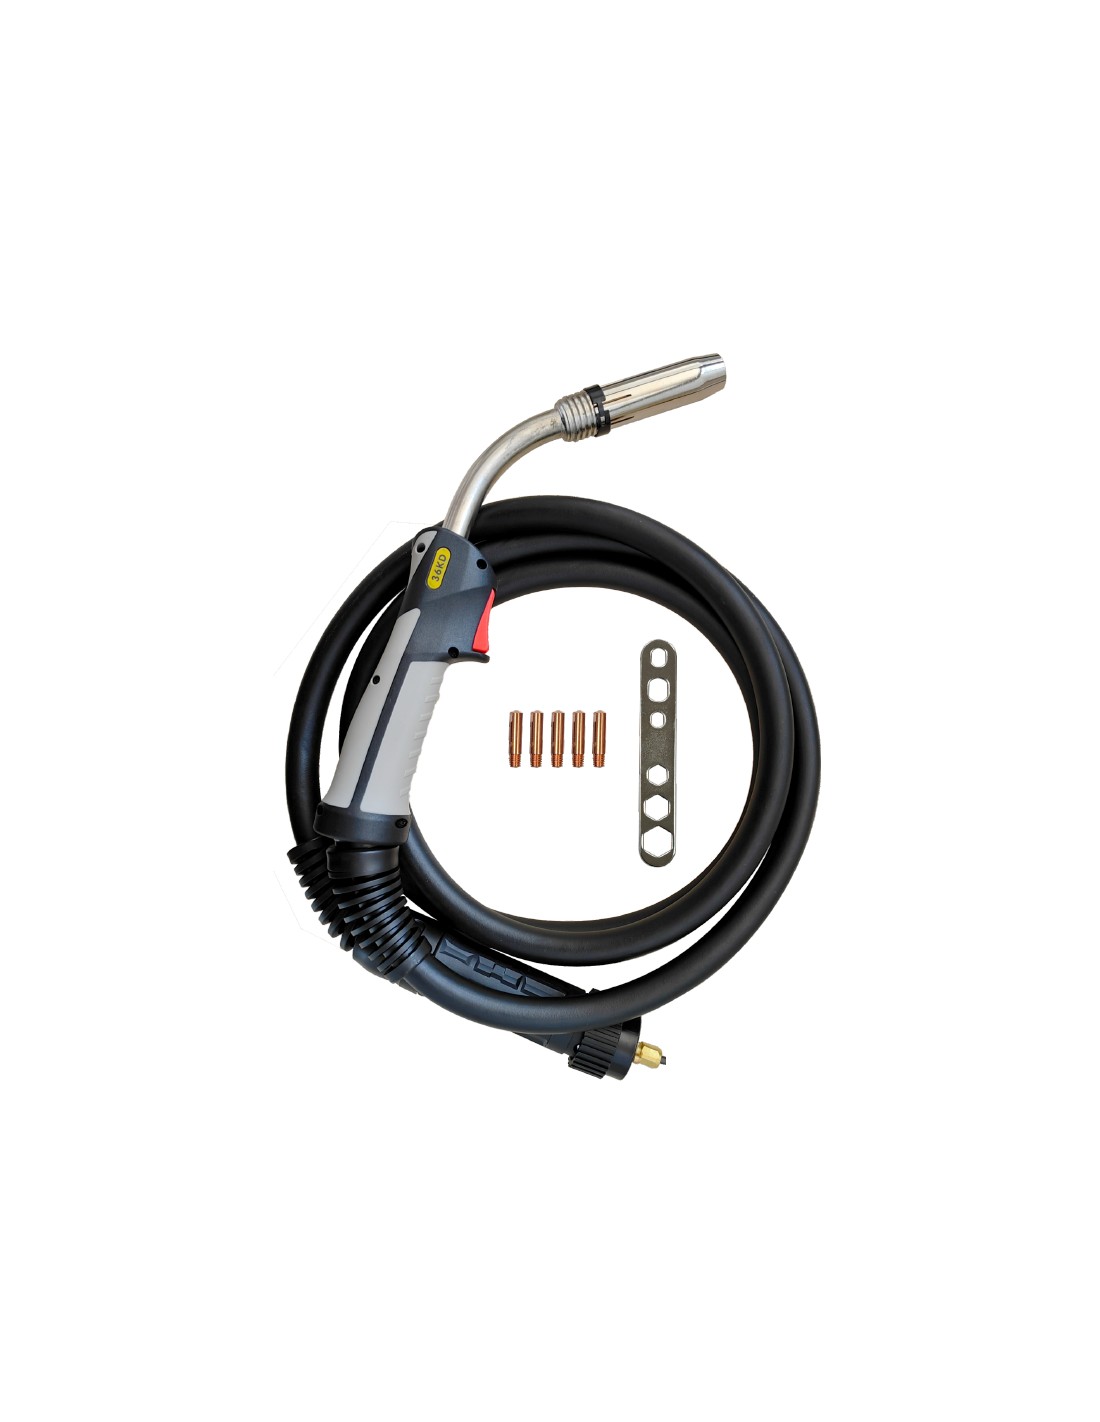
The standard EURO connector for the MIG torch combines welding current, gas, wire feed and control contacts in a single connection. The torch can be quickly connected, disconnected or easily replaced with another compatible MIG torch, and the threaded lock ensures a secure connection during operation.
FORBY welding equipment focuses on quality, durability and ease of use, which is why even compact machines feature higher-specification solutions such as large 35-50 cable connectors and a universal EURO connector for the MIG torch.

Important before starting work
- Check the power supply. A three-phase 400 V supply is required. The power line and its protection must match the machine's load and the manufacturer's connection requirements.
- Match the wire and feed parts. Select rollers, liner and contact tip suitable for the wire material and diameter.
- Set the correct polarity. Follow the wire or electrode manufacturer's instructions. Disconnect the machine from the mains before changing connections, the spool or rollers.
- Select the right program. Material, wire diameter and gas settings must match the consumables used. Start with a test weld on a scrap piece of the same material.
- Prepare the workpiece. Clean the welding area and the earth clamp attachment point, and ensure reliable electrical contact.
- Ensure cooling. Observe the duty cycle. If the overheating protection activates, stop welding and let the machine cool down with the fan running.
- Use welding protective equipment. Ensure proper ventilation, remove flammable materials and protect the machine from rain and moisture.

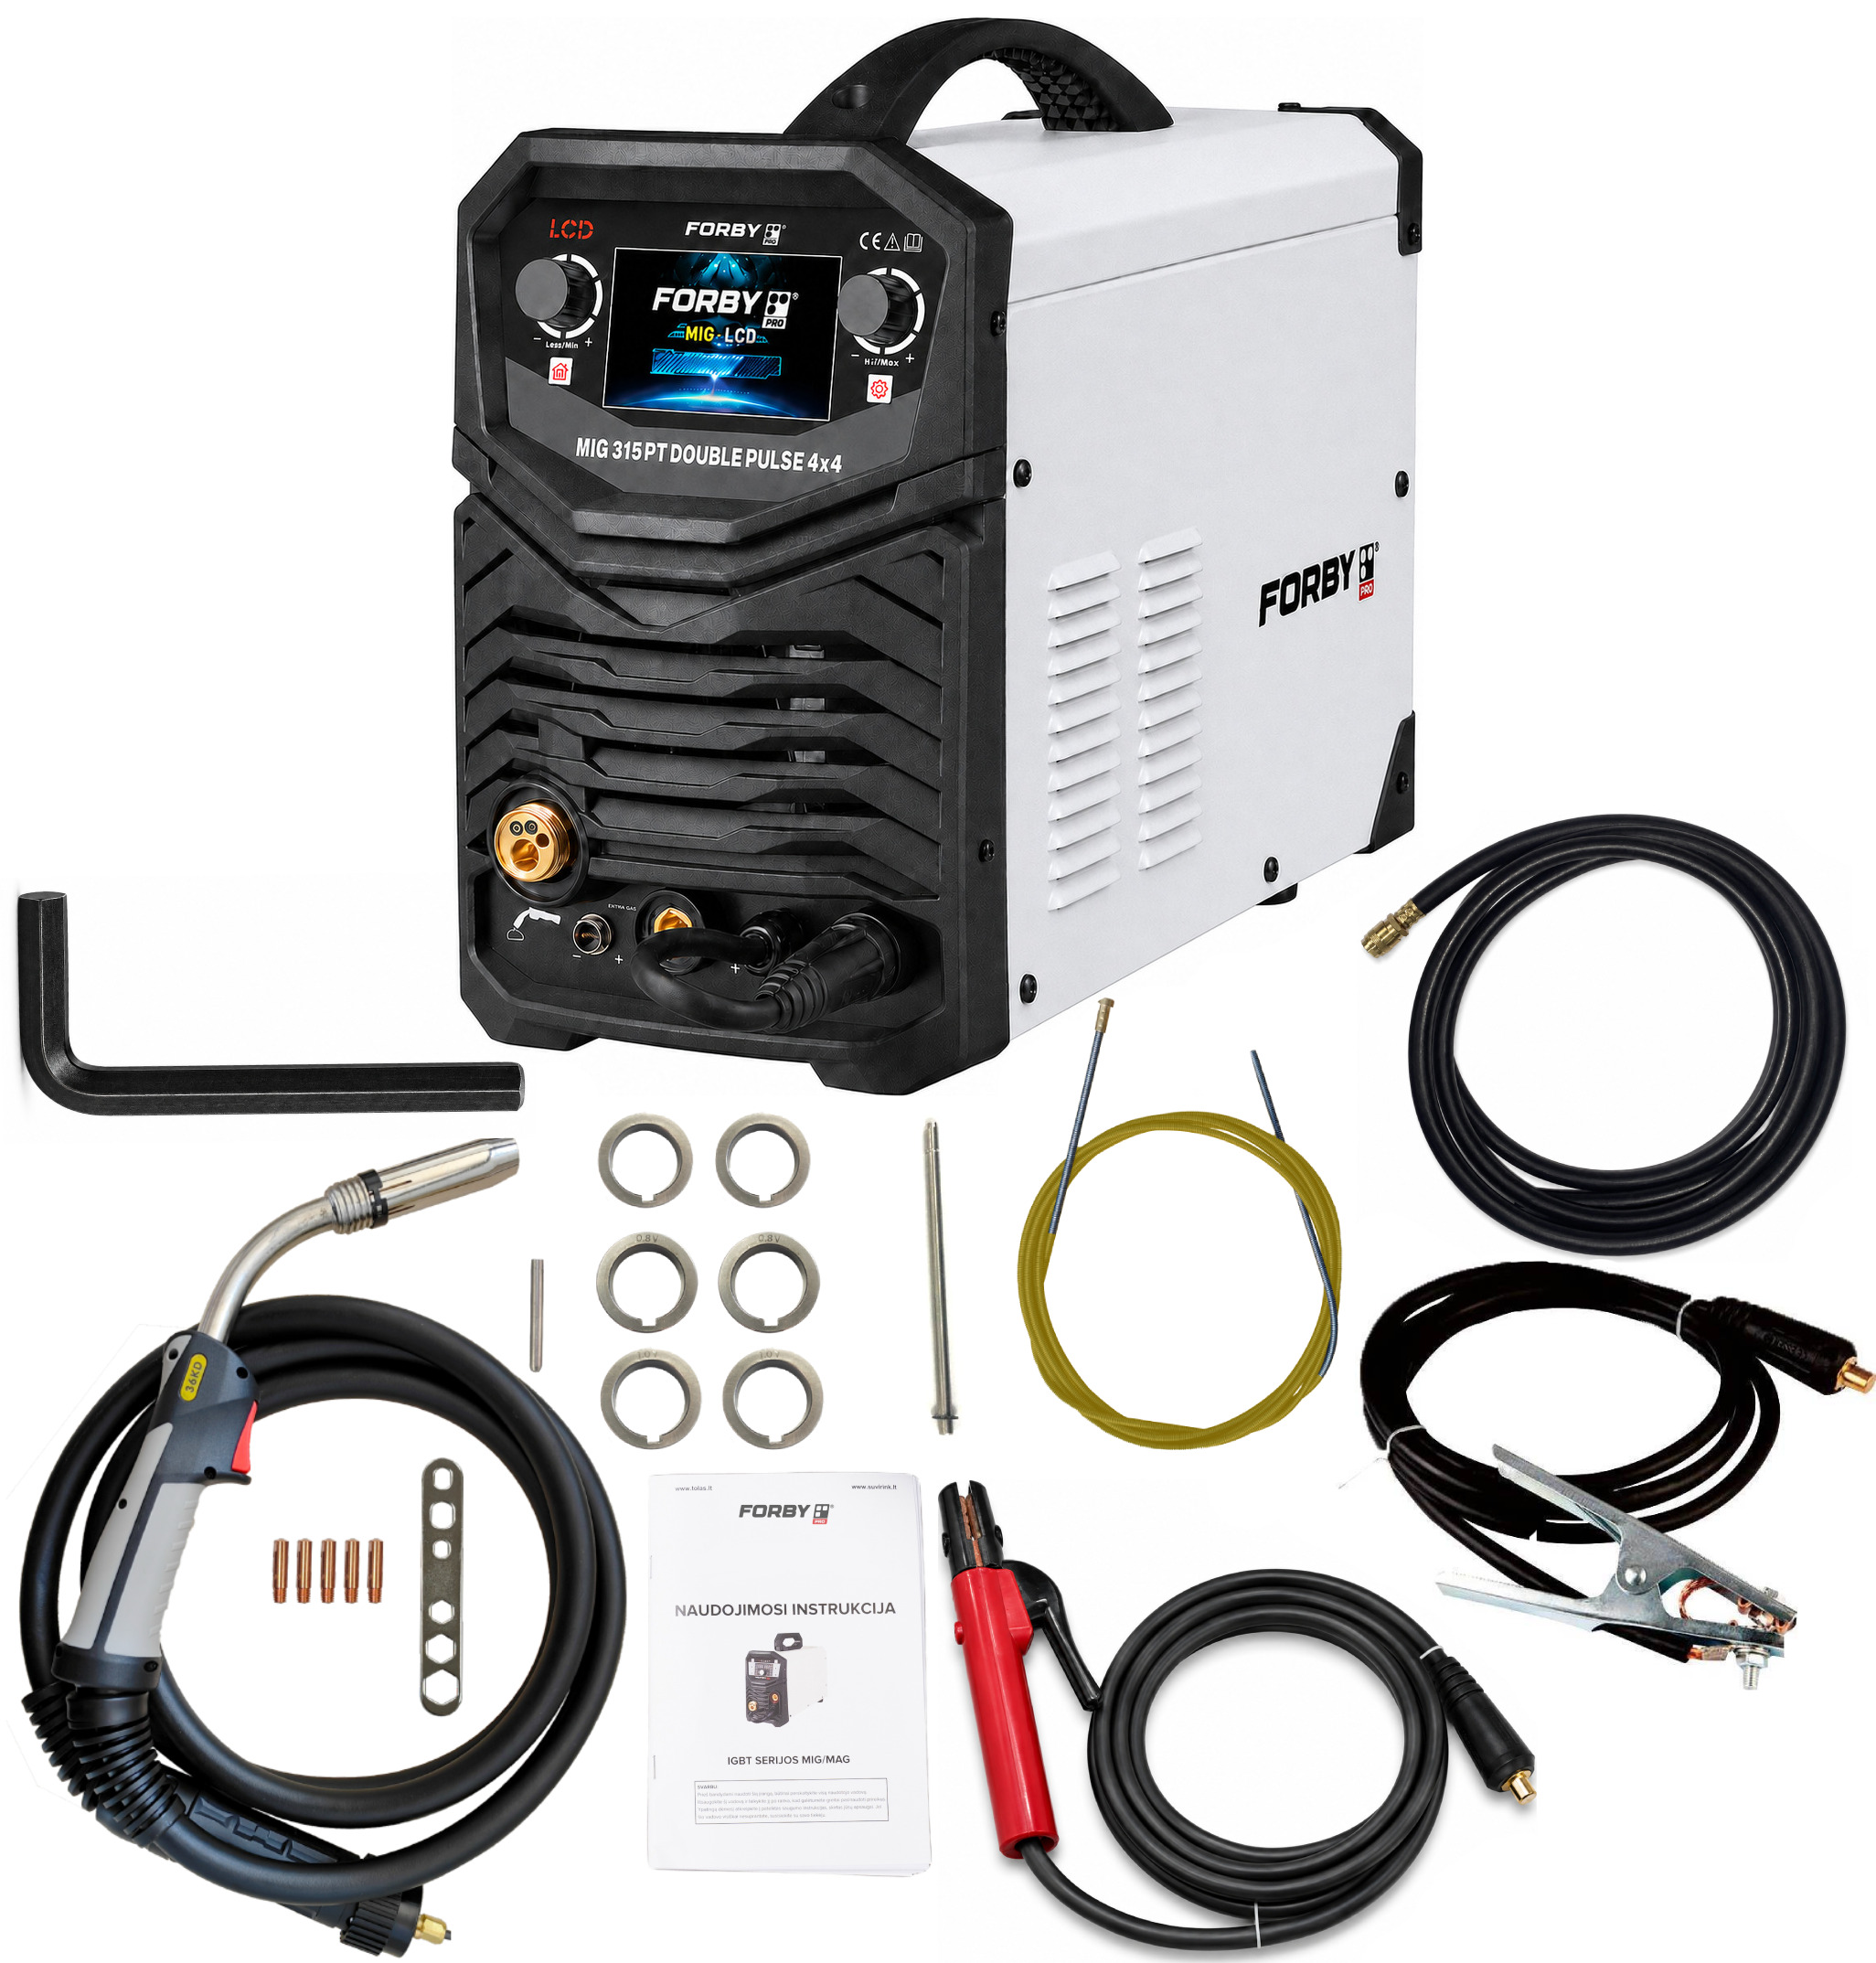
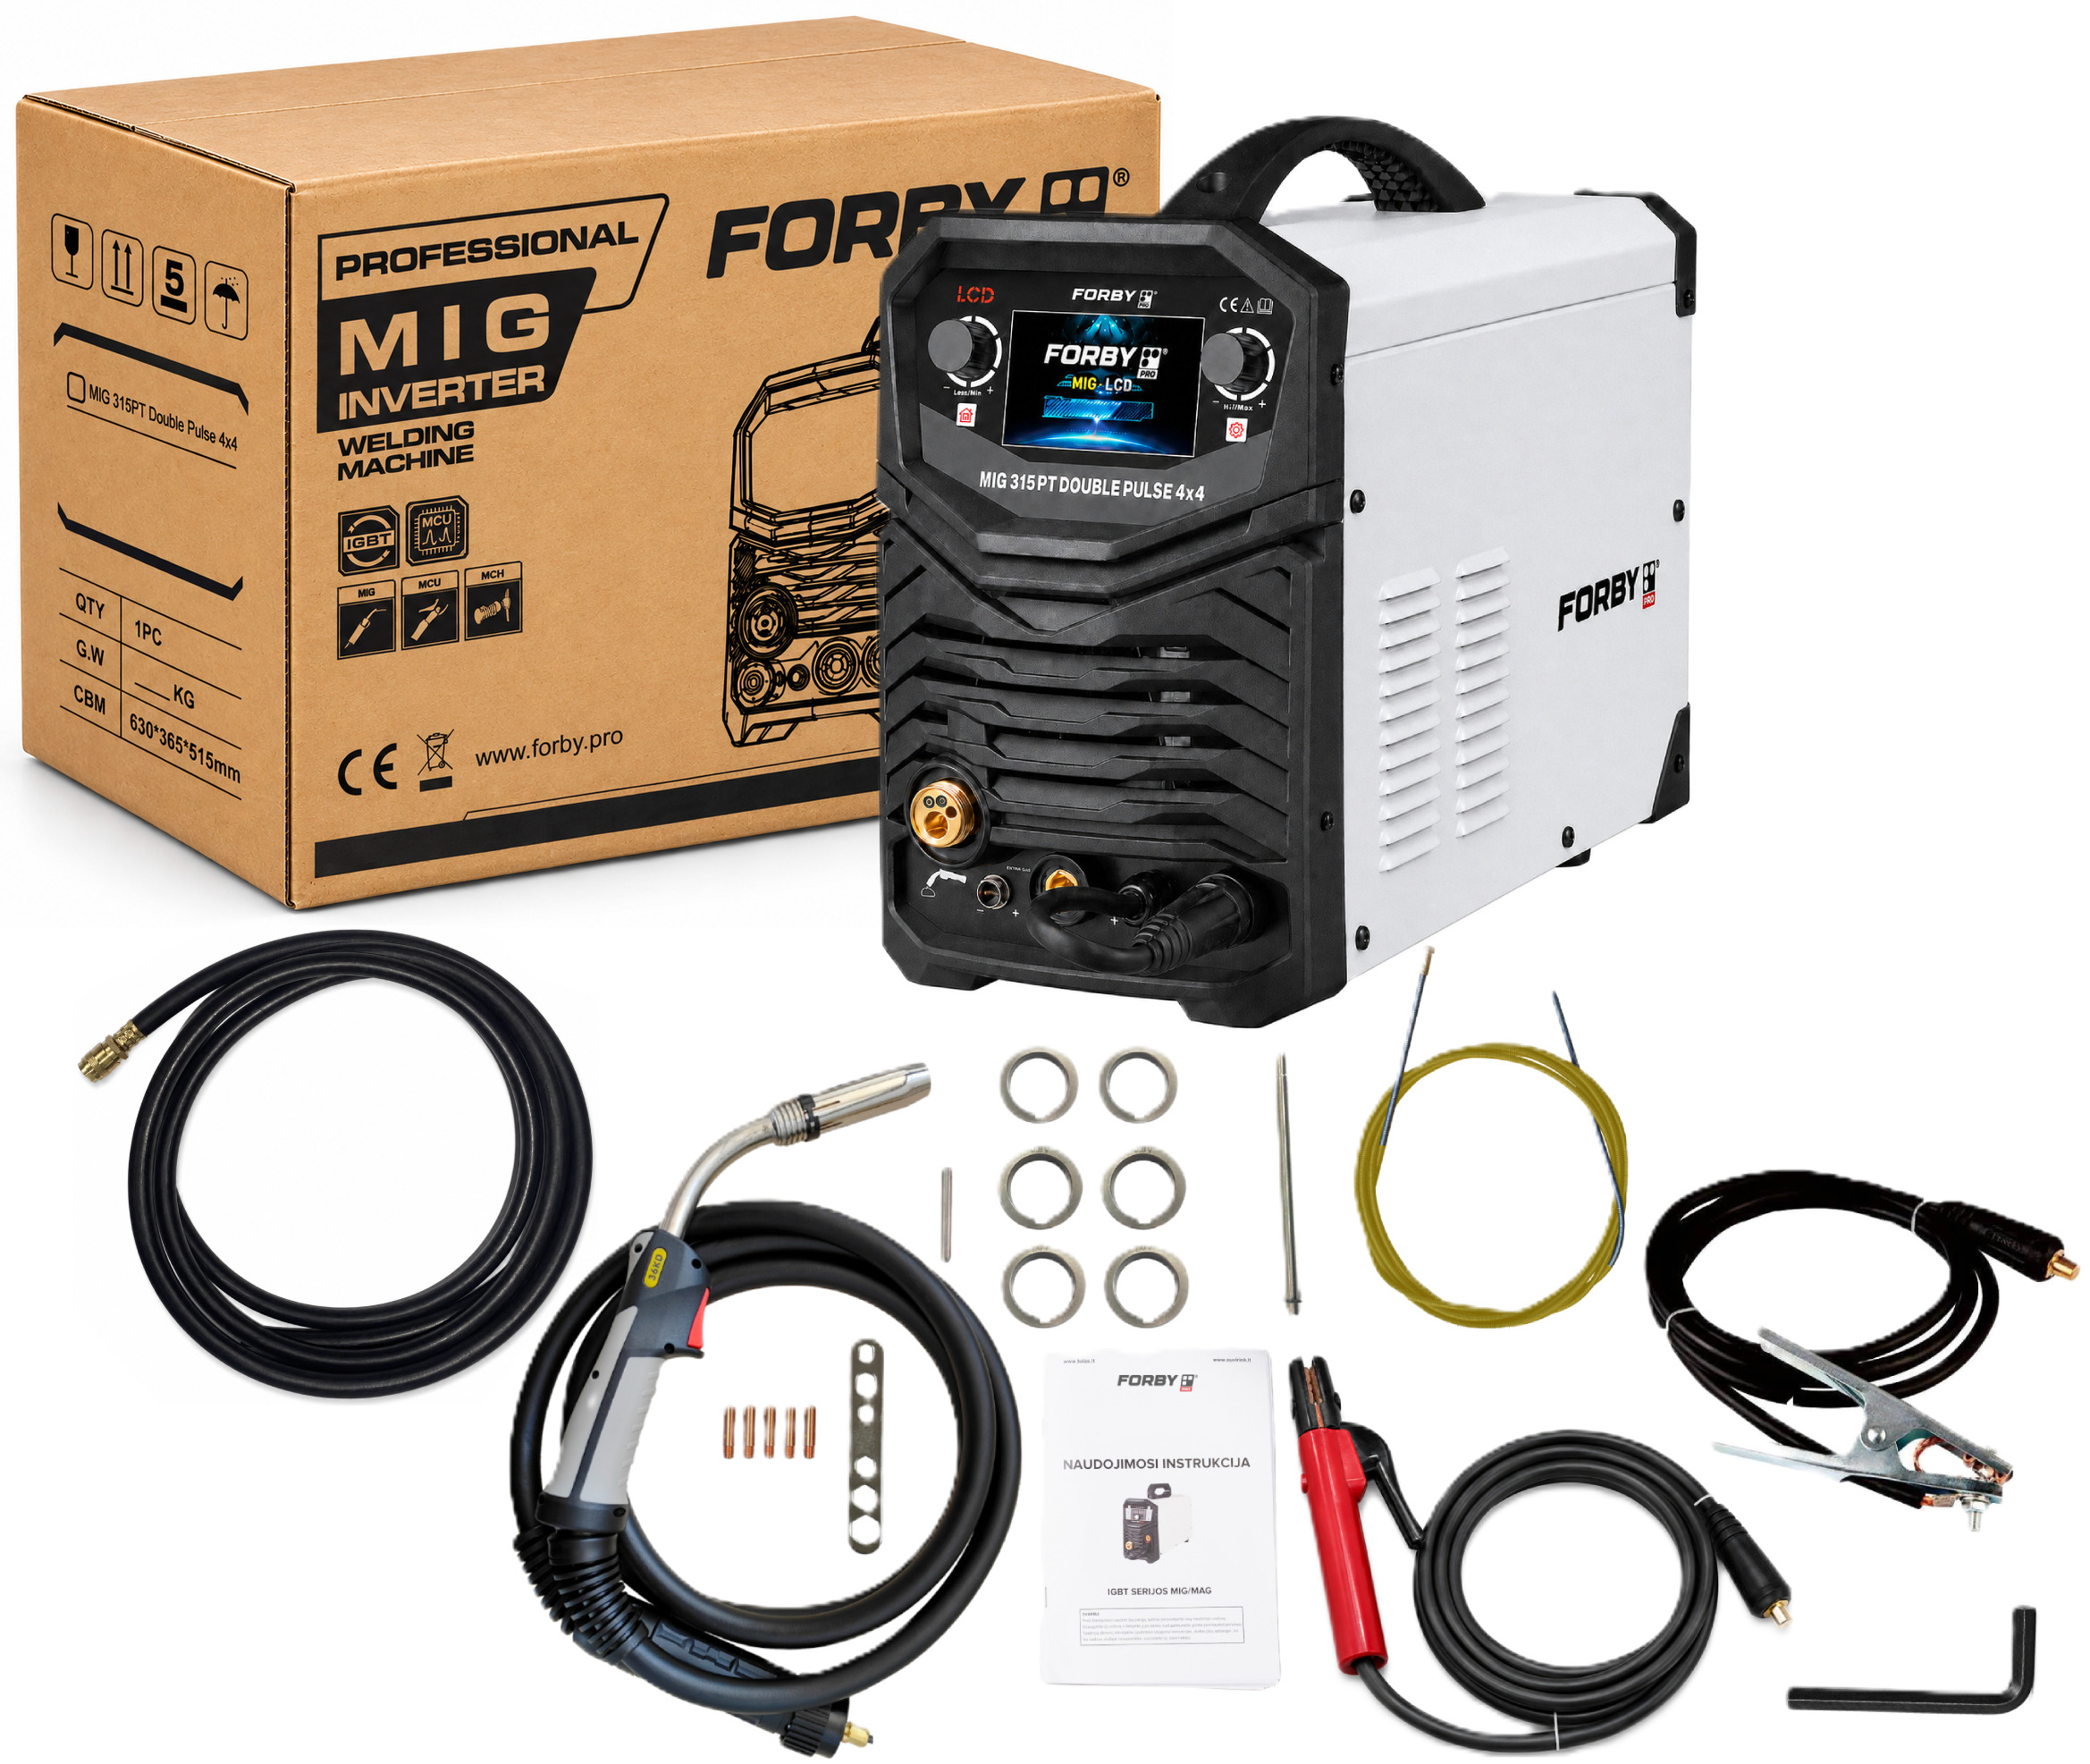
Package contents
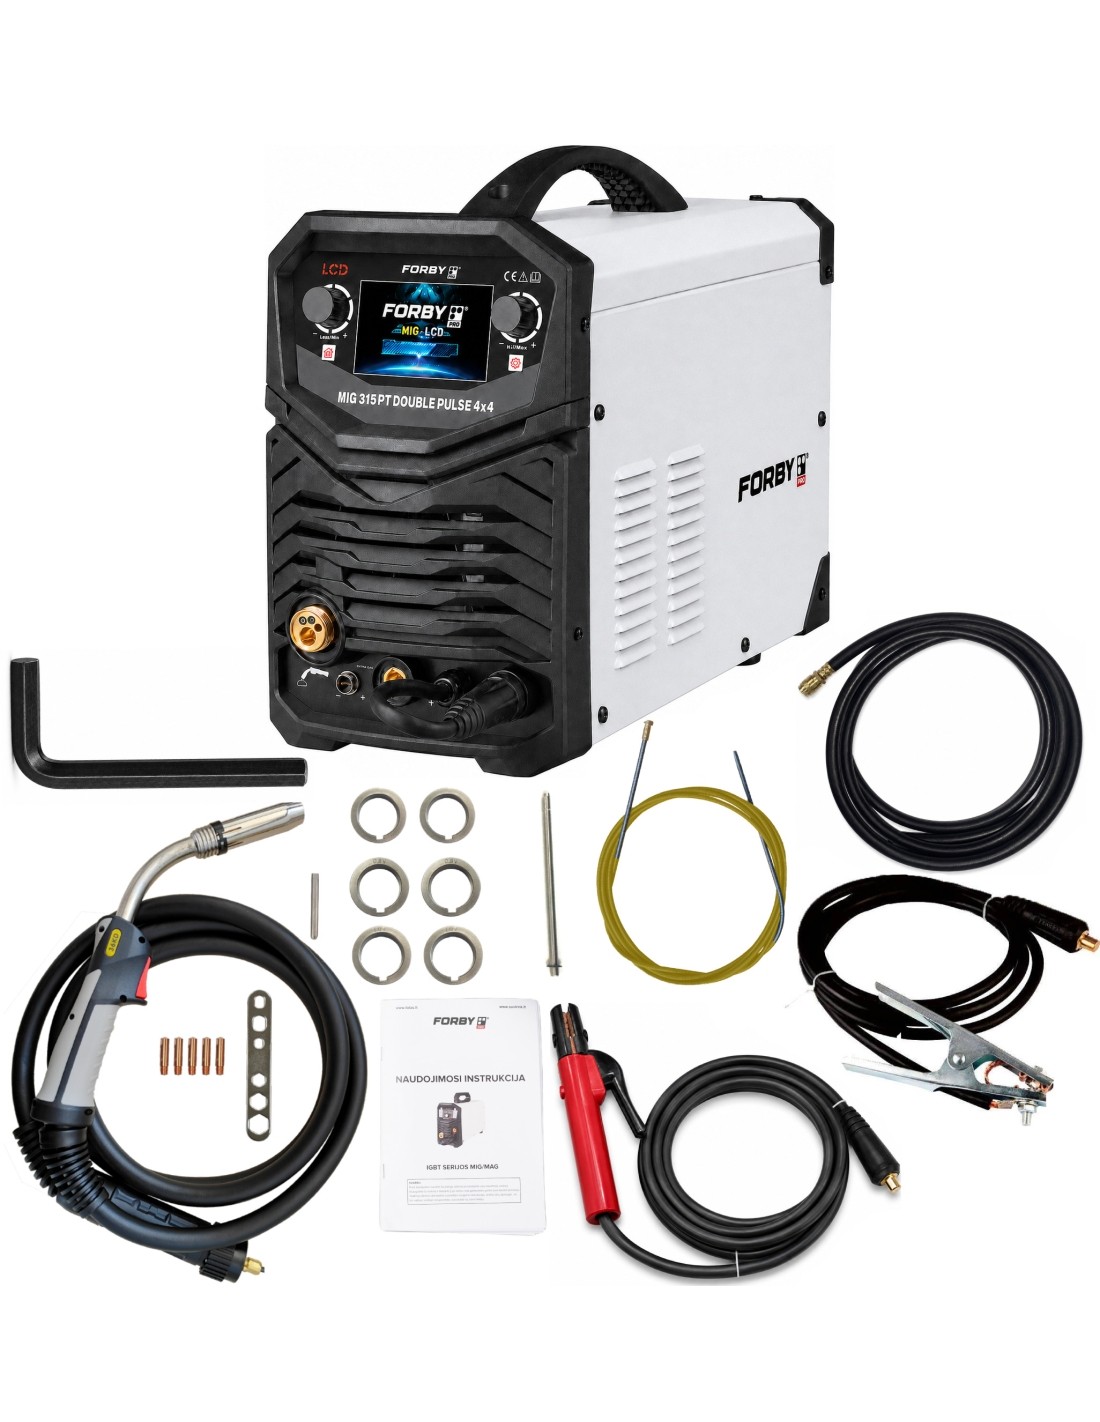
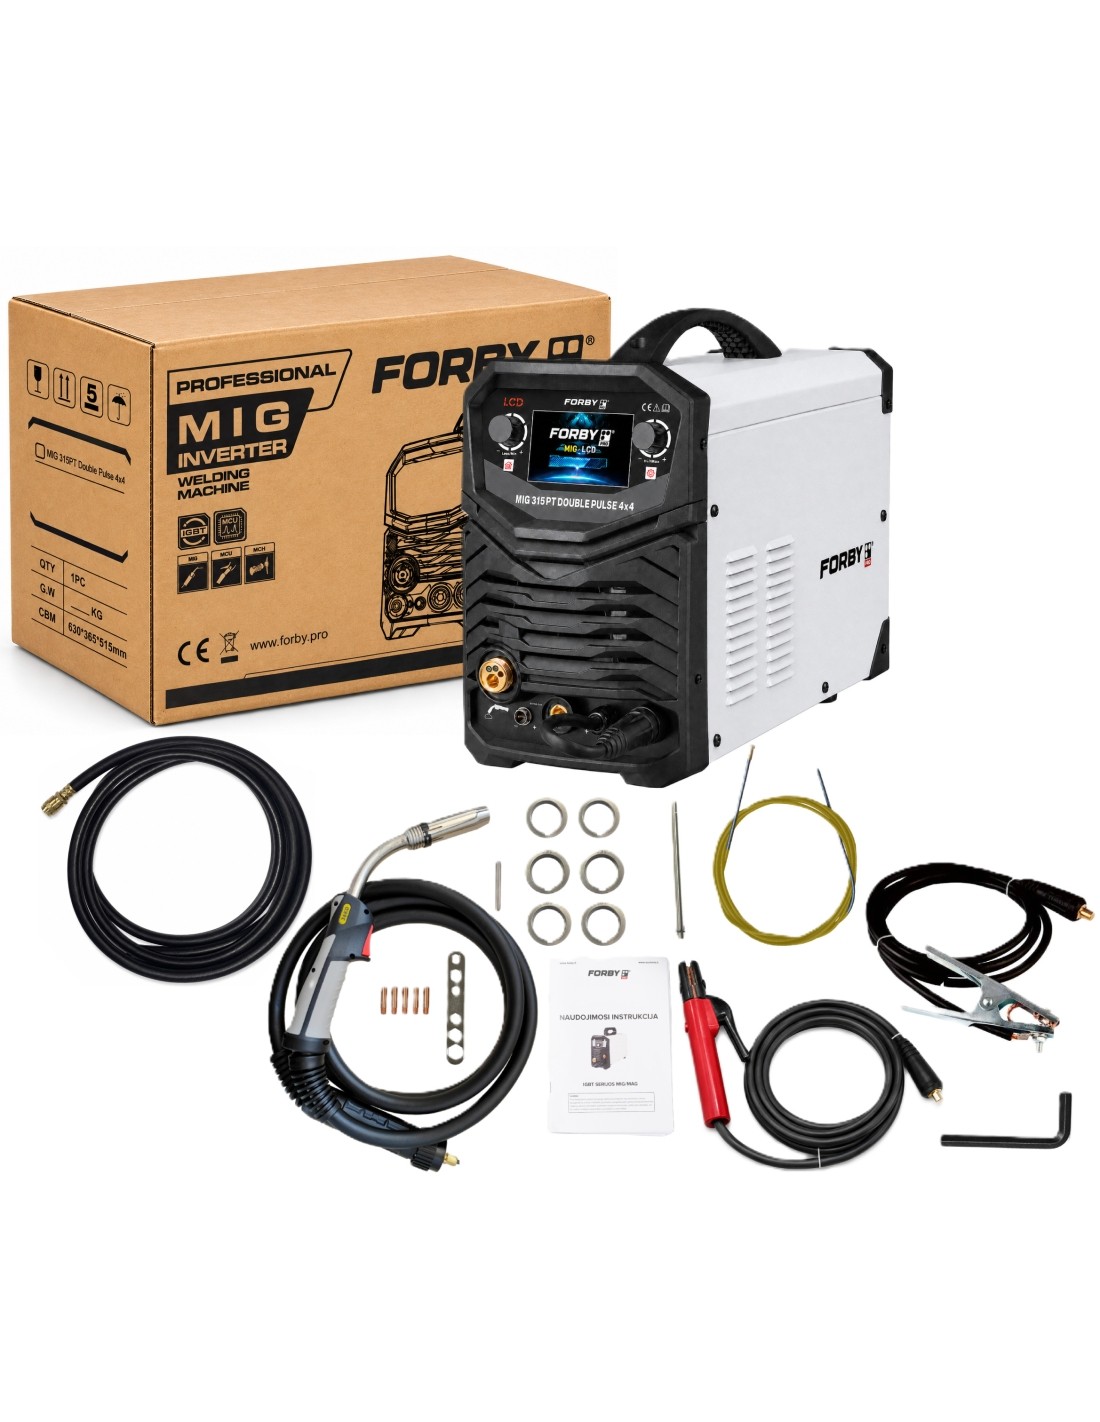
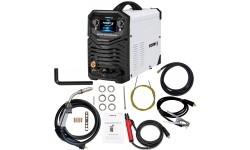
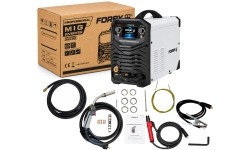
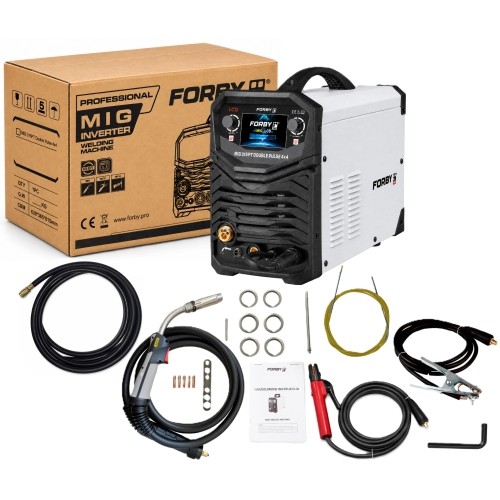
- Welding machine FORBY® MIG 315PT Double Pulse 4x4.
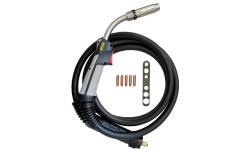
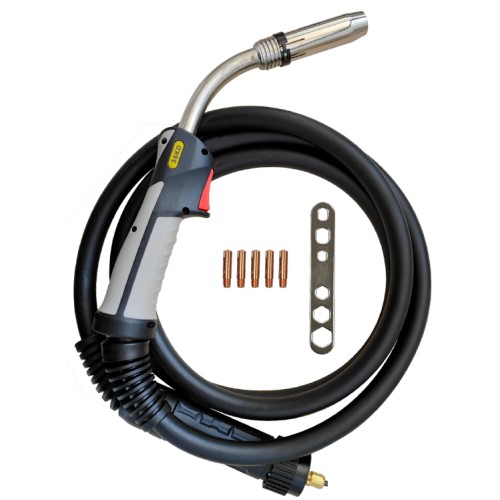
- MIG torch 36KD, 3 m, with EURO connector, fitted 1.0 mm contact tip and steel liner (for steel).
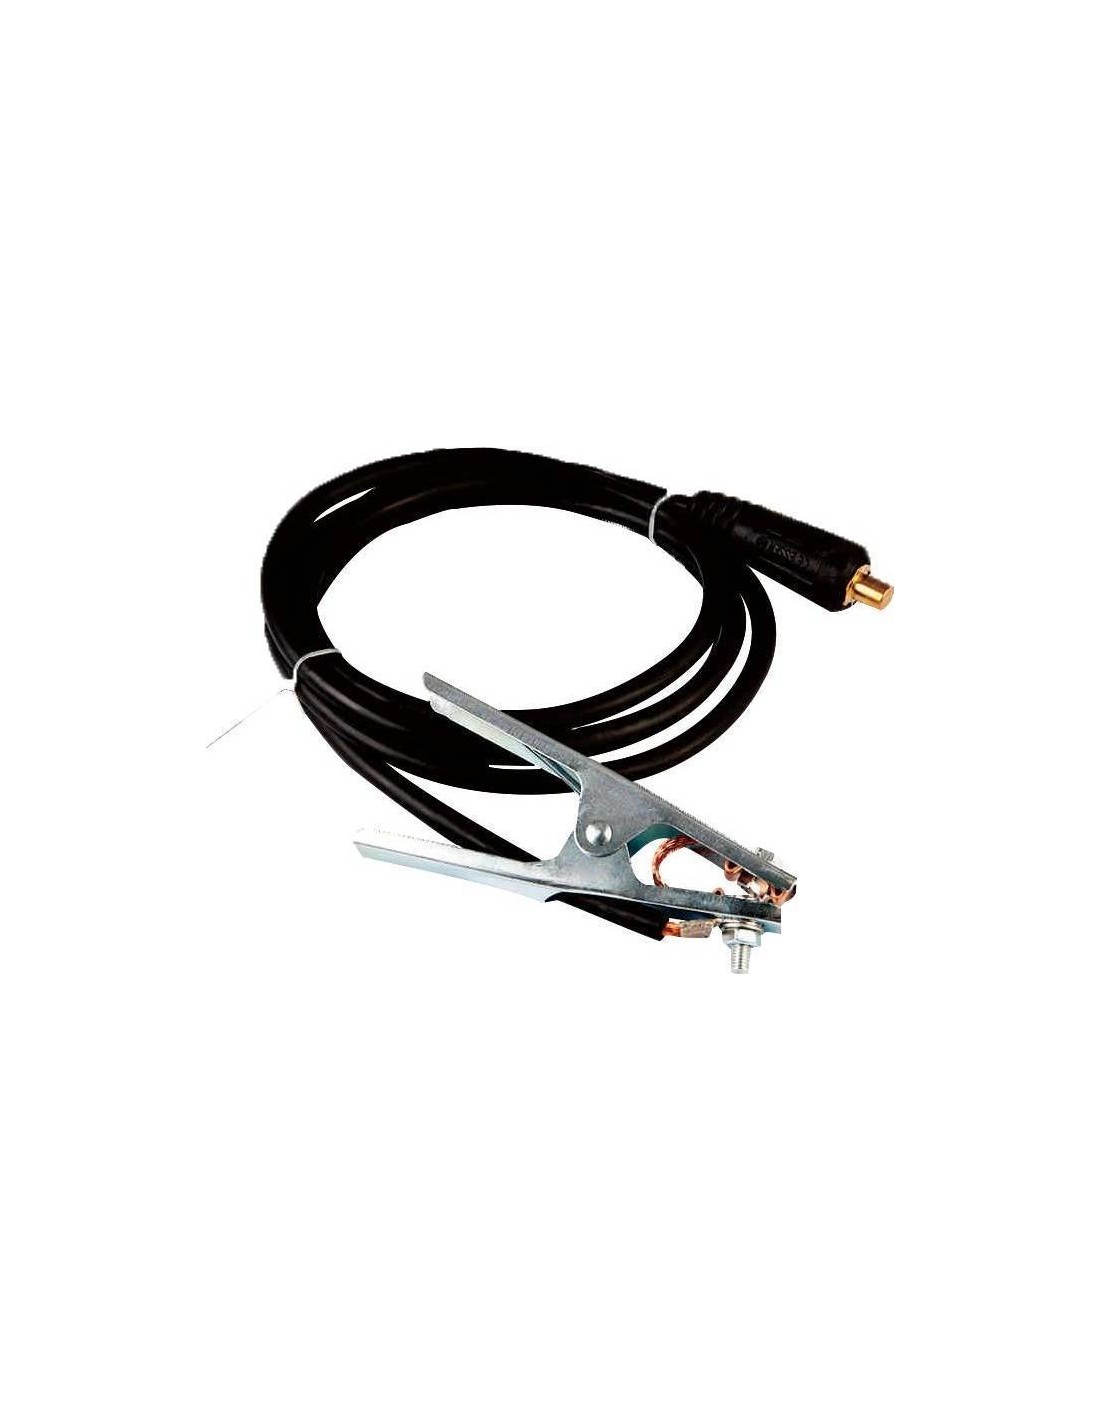
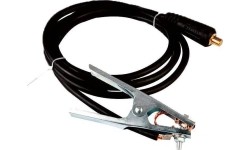
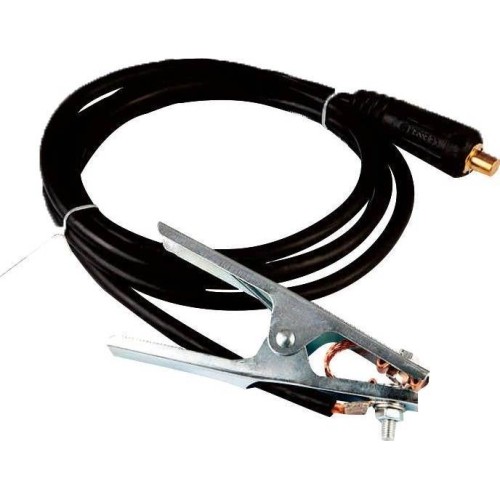
- 300 A earth clamp with 3 m cable - 35 mm² copper conductor, 35-50 type plug.
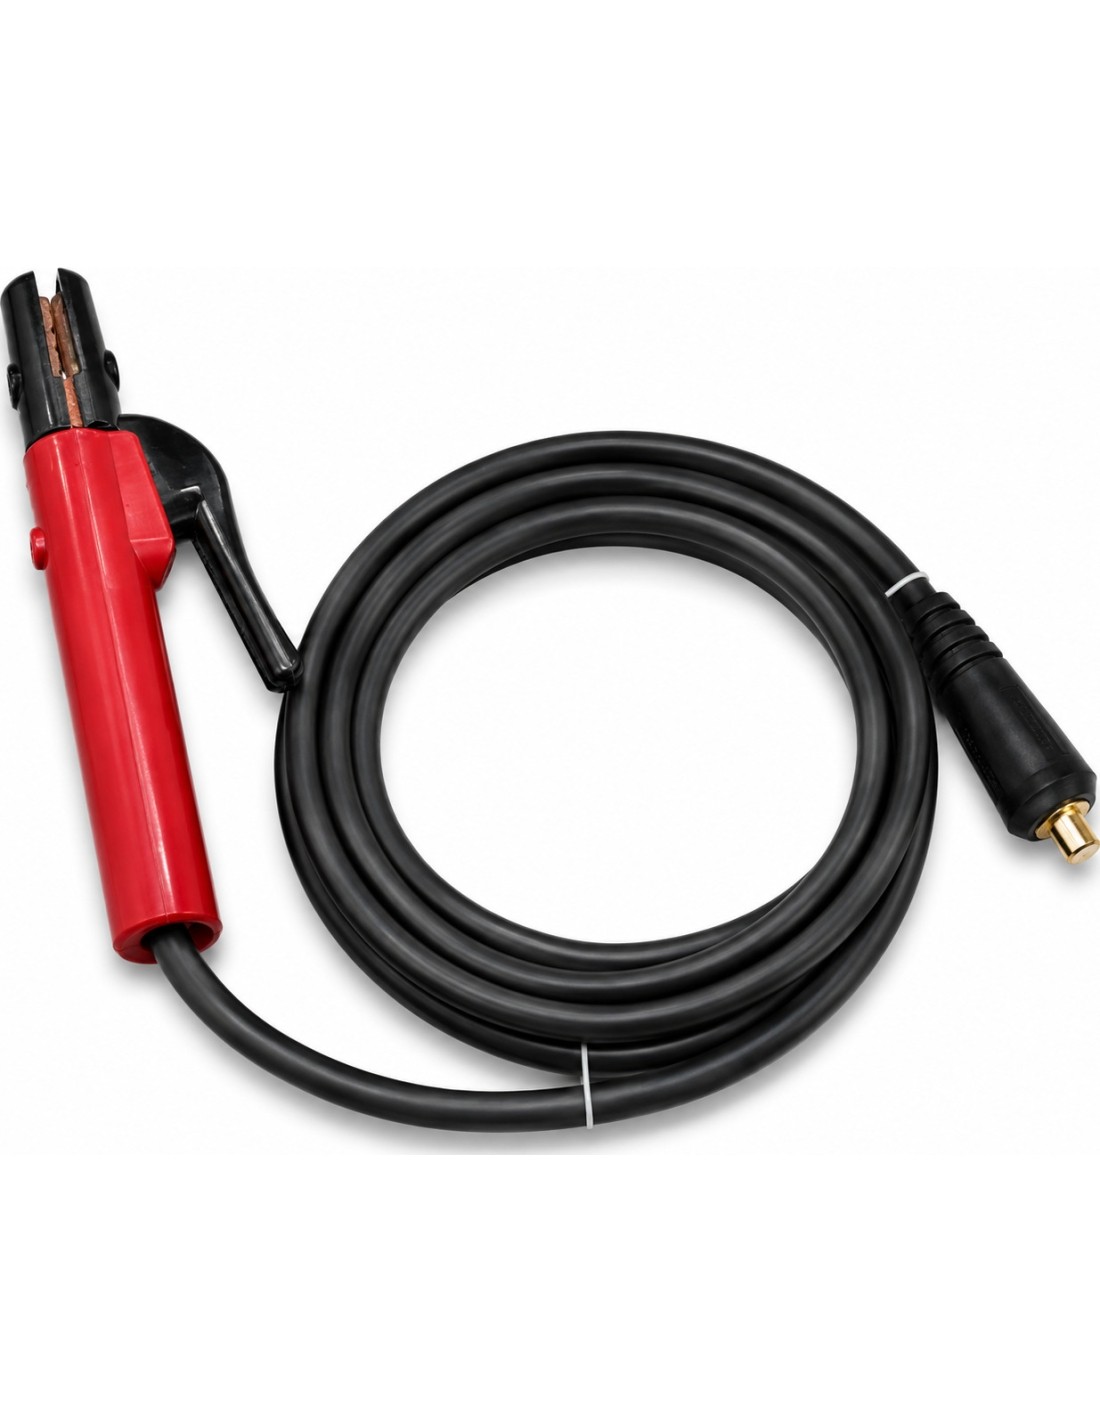
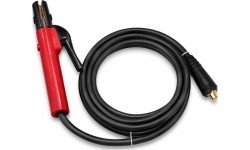
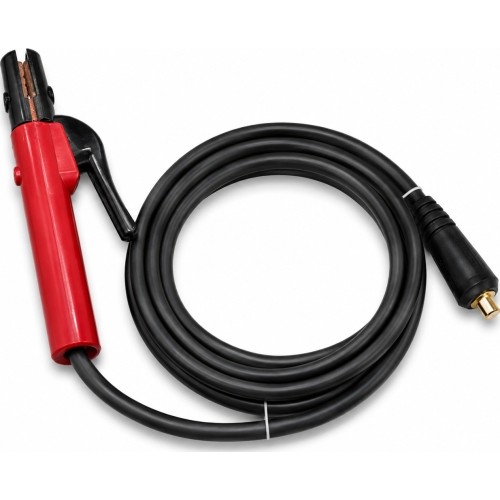
- 600 A electrode holder with 3 m cable - 35 mm² copper conductor, 35-50 type plug.
- Gas hose, 3 m, with NW5 quick coupling and 1 clamp; inner diameter - 6 mm, outer - 13 mm.
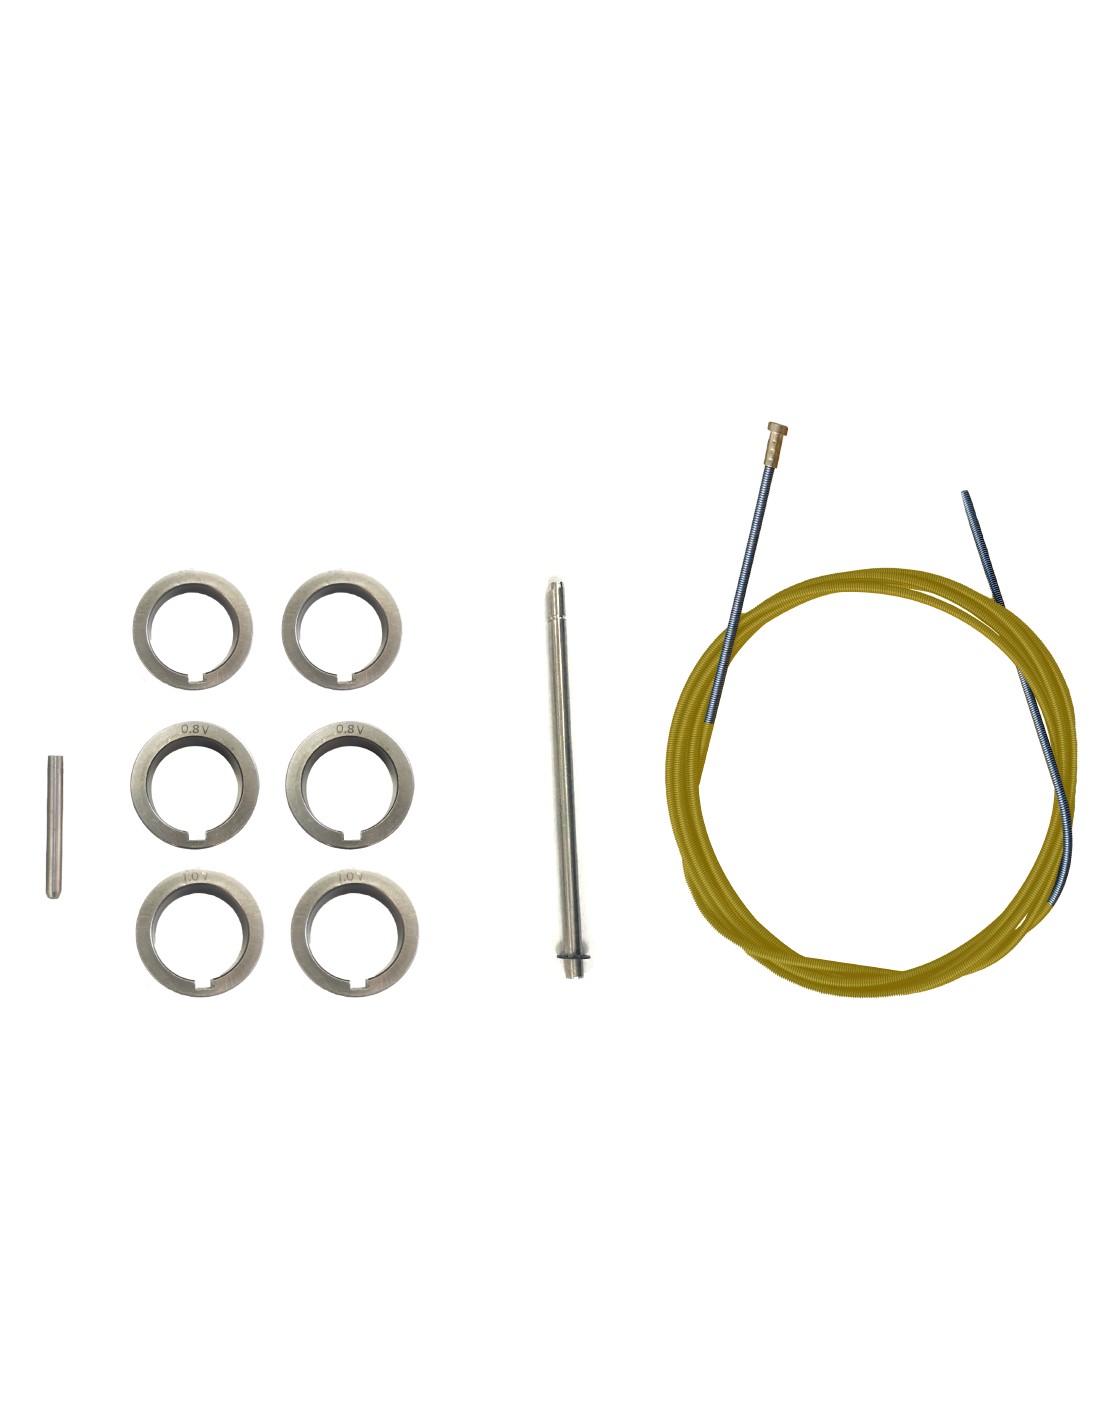
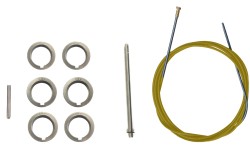
- 2 V-groove rollers 0.8-1.0 mm and pressure rollers - fitted in the wire feed mechanism.
- 2 additional V-groove rollers 1.0-1.2 mm - for steel wire.
- 4 additional U-groove rollers 1.0-1.2 mm - for aluminium wire.
- Wire feed mechanism inlet guide and EURO connector wire guide.
- Teflon liner (for aluminium) - 1 pc.
- Additional contact tips: 0.8 / 1.0 / 1.2 mm - 1 pc each.
- Additional contact tips for aluminium wire: 1.0 / 1.2 mm - 1 pc each.
- Torch maintenance wrench - 1 pc.
TIG torch is not included. For Lift TIG work, a compatible torch, argon gas supply, regulator and consumables are additionally required.
FORBY® MIG 315PT Double Pulse 4x4 - power and precise welding control
Synergic control simplifies setting selection, the four-roller mechanism helps feed the wire evenly, and double pulse gives more options for controlling bead shape and heat input.
300 A / 60 % MIG and Lift TIG • 400 V • Double Pulse • 4x4 • 5″ LCD • EMC
About FORBY®
Forby is an engineering-driven company dedicated to creating professional welding equipment that meets the highest standards of precision, reliability, and safety. Founded by experts with decades of experience in industrial fabrication, Forby has grown into a trusted partner for manufacturers, construction firms, and workshops across Europe.
Our mission is simple — to empower welders with tools that make their work faster, safer, and more accurate. Every machine and accessory we build goes through rigorous testing to ensure long-term performance in the most demanding conditions.
With a focus on innovation, user comfort, and durability, Forby continues to push the boundaries of what’s possible in modern welding technology.